Prusa
  • SHOP
    • Latest products
    BY CATEGORY
    • 3D printersnew
    • 3D printer upgradesnew
    • Materials
    • Accessories
    • Spare parts
    • Courses
    • Merch
    • Get a price quote
    QUICK LINKS
    • Shipping & delivery
    • Returns & refunds
    • Payment & financing
    • Warranty
    • VAT & Customs fees
    • FAQ

    0 item in your cartitems in your cart

    Your cart is empty

    Go to cartShop 3D printers

    My profile

    Log in to see orders, saved items

    My profile

    Signed in as

    • Orders
    • Logout
  • 3D PRINTING
    • Explore 3D printing
    FOR BEGINNERS
    • 3D printing 101
    • How FDM printing works
    • Buying your first printer
    • 3D model catalog
    BY APPLICATION
    • Rapid prototyping
    • Manufacturing
    • Engineering
    • Research
    • Arts & design
    GO DEEPER
    • Materials guide
    • Courses
    • Webinars
    • Case studies
    • Custom 3D printing
  • 3D PRINTERS
    • All 3D printers
    FOR
    • Home or garageHobbyists, tinkerers and home printing
    • BusinessIn-house production for small teams
    • EnterpriseFleets, security and scale
    • Which Prusa is right for me
    SHOP & BROWSE
    • CORE One+new
    • CORE One+ INDXnew
    • CORE One L+new
    • CORE One L+ INDXnew
    • XL+new
    • MK4S
    • Prusa Pro HT90
    • Prusa Pro AFS
    • Prusa Pro SLX
    MORE FROM PRINTERS
    • Parts & upgradesnew
    • Critical infrastructure
    • Case studies
    • Signature Oak
    • Kits
  • MATERIALS
    • All materials
    BY USE
    • Every-day & design
    • Functional engineering
    • Composites
    • Pro speciality
    • SLA resins
    PRUSAMENT
    • PLA
    • PETG
    • ASA
    • PC
    • PA11
    • Flex
    • TPU
    MORE FROM MATERIALS
    • Materials guide
    • We make material in house
    • Sustainability
    • Order on the store
  • SOFTWARE
    • All software
    PREPARE THE PRINT
    • PrusaSlicer 3.0New
    PRINT & MONITOR
    • Prusa Connect
    • EasyPrint
    • iOS & Android app
    • Prusa Farm
    GET STARTED
    • Download & install
    • Knowledge base
    MORE FROM SOFTWARE
    • 3D model catalog
  • SUPPORT
    • Explore support
    FIND ANSWERS
    • Knowledge base
    • Troubleshooting
    • Courses
    • Webinars
    GET HELP
    • Contact us
    • Livechat
    • Shipping & delivery
    • Warranty
    • Returns & refunds
    • Service & spare parts
    • Service & Repair
    COMMUNITY
    • Forum
    • Reddit
    • Printables
  • TRUST CENTER
    • Trust Center overview
    BY TOPIC
    • GDPR
    • Certificates
    • Security
    • Compliance
    COMMITMENTS
    • Sustainability report
    TALK TO US
    • Contact the security team
  • COMPANY
    • About Prusa
    GET TO KNOW US
    • Our story
    • How we make printers
    • Open source
    • Brand & media kit
    NEWS
    • Blog
    • Newsroom
    • Events
    TRUST & PARTNERS
    • Sustainability
    • Resellers & distributors
    • Affiliate program
    • Contact
    • English
    • Čeština
    • Deutsch
    • Español
    • Français
    • Italiano
    • Polski
    • 日本語
  • Signed in as

    • Orders
    • Address
    • In-stock Alerts
    • My Courses
    • Subscription
    • Edit Account
    • Logout

Log in to see orders, saved items

Signed in as
  • Orders
  • Address
  • In-stock Alerts
  • My Courses
  • Subscription
  • Edit Account
  • English
  • Čeština
  • Deutsch
  • Español
  • Français
  • Italiano
  • Polski
  • 日本語
Shop

0 item in your cartitems in your cart

Your cart is empty

Go to cartShop 3D printers

My profile

Log in to see orders, saved items

My profile

Signed in as

  • Orders
  • Logout
SHOP
  • Latest products
BY CATEGORY
  • 3D printersnew
  • 3D printer upgradesnew
  • Materials
  • Accessories
  • Spare parts
  • Courses
  • Merch
  • Get a price quote
QUICK LINKS
  • Shipping & delivery
  • Returns & refunds
  • Payment & financing
  • Warranty
  • VAT & Customs fees
  • FAQ

Featured products

    Popular categories

      Trending searches

        Articles

          Blog

            Products

              Categories

                Suggested searches

                  Searching…
                  No results
                  Something went wrong.
                  ↑↓ Select↵ OpenEsc Close search
                  1. Support
                  2. Original Prusa i3 MK2S
                  3. Material guide
                  4. Drying filament
                   

                  Contents

                  • Prevention
                  • Multi-Tool Printing
                  • How to recognize if the filament has gathered humidity
                  • Prusament spool types
                  • Drying methods

                  Blog

                  • Print colorful and glowing Halloween decorations with our spooky offer
                  • Factorio Has Arrived on Printables
                  • Prusament PLA Lightweight: 65% lighter than regular PLA. Perfect choice for aircraft, cosplay, and more.

                  Newsletter

                  Signup and get our monthly squeeze on updates, blog, printables and much more.

                  By clicking, you agree to receive our newsletter.

                  This site is protected by reCAPTCHA Enterprise and the Google Privacy Policy and Terms of Service apply.

                  Factorio Transport Belts
                  E-shop
                  • 3D Printers
                  • Printer Upgrades
                  • Filaments
                  • Accessories
                  • Prusa Merchandise

                  © Prusa Research a.s.

                  Printables
                  • 3D Models
                  • Store
                  • Clubs
                  • 3D Design Contests
                  • Brands
                  Community
                  • World Map
                  • Forum
                  • User Groups
                  • Events
                  Help
                  • Prusa Help
                  • Prusa Academy
                  • 3D Printing Calculators
                  Software
                  • PrusaSlicer
                  • Prusa.app
                  • Prusa Connect
                  • Drivers and Software
                  Company
                  • About Us
                  • Blog
                  • Official Prusa Resellers
                  • Contact Us
                  • Certified for ISO 9001, ISO 14001, ISO 45001
                  • General Terms and Conditions
                  • General Terms and Conditions of Use of the PRUSA Websites
                  • Privacy Policy
                  • Information about cookies
                  • Customer Complaints Policy
                  • Status Page
                  • Do Not Sell or Share My Personal Information
                  • Supplemental Statements

                  © Prusa Research a.s.

                  JOSEF PRUSA®, PRUSA RESEARCH®, PRUSA POLYMERS®, PRUSA ORANGE®, PRUSA 3D ® AND PRUSAMENT® are registered trademarks of Prusa Development a.s. used by Prusa Research a.s. under licence from Prusa Development a.s.

                  Drying filament

                  Relevant for

                  MK4 family
                  XL family
                  MMU family
                  PRO family
                  MINI family
                  +
                  27 comments
                  Article is also available in following languages
                  English
                  Čeština
                  Polski
                  Deutsch
                  Français
                  Español
                  Italiano
                  日本語

                  The materials used for FFF 3D printing are mostly hygroscopic. This means that they readily attract water molecules from the environment they are in. When used for printing, a material that has gathered humidity might not behave as expected.

                  Prevention

                  Some filaments are more hygroscopic than others. When using a new material, make sure to research its properties and the best way to store it. It is best to avoid having to dry the filament if possible.

                  It is best to store your filaments in a closed space or box, with some desiccant material in it. If you have limited availability for this type of storage, prioritize storing filaments that are more hygroscopic. PLA, for example, doesn't change properties too much by uptaking humidity, whereas Polyamide is affected quite significantly.

                  To prevent any issues with the highly hygroscopic materials (polyamide, polypropylene, PVA, BVOH, ...), it is recommended to either ensure they are stored in a dry environment or dry them before every print.

                  You can purchase a box with the specific purpose of keeping the filament dry (such as Prusa USS Drybox), or make your own.

                  Another popular solution to keep your filament dry is using vacuum bags for storage. There are bags specific for filaments, but you can use any that will fit a filament inside. Keep a desiccant in the bag when storing the filament.

                  Multi-Tool Printing

                  In printers like the Original Prusa XL, where filament is loaded directly into toolheads, any humidity in the filament is critical. When printing with multiple toolheads, the unused tools remain heated (the idle temperature is set to 70°C by default). If the filament is wet, moisture is released into the tool, causing stringing in the toolhead. In such cases, even PLA can absorb enough moisture to create printing issues. This makes the XL more susceptible to filament moisture compared to single-tool printers, therefore we recommend drying the filament before printing on the Original Prusa XL.

                  How to recognize if the filament has gathered humidity

                  In case a material is affected by humidity, the general first signal will be a poor quality of the model surface.

                  Some filaments are naturally more stringy than others. Make sure to compare different results from your prints, and check our Stringing and oozing guide.

                  In some cases, the high content of water in the filament can cause low layer adhesion, blobs on the prints, and bubbling and smoke during extrusion.

                  Polyamide, PVA, and TPU (Flex) are filaments more often in need of drying than more popular filaments like PLA.

                  Prusament spool types

                  Prusament filaments are wound on a redesigned spool that introduces several improvements for an even better printing experience, starting in October 2025. The new spool features a simple locking mechanism that makes disassembly quick and easy, allowing effortless refills. It also stays secure during filament drying, even at higher temperatures.

                  For standard (low-temperature) filaments, we use a black spool, which resists drying temperatures as high as 90 °C. And for high-temperature filaments (Prusament PEI 1010), we use a grey spool, which is usable for temperatures reaching 150 °C. The new spools don't require any extra preparations before drying.

                  However, there is still a significant number of old spools on the market, which need extra preparation before drying filament.

                  Prusament black spool (old version)

                  The black plastic sides of Prusament spools are firmly pressed into the cardboard cylinder. The plastic sides expand with rising temperature and cause the expansion of the cardboard center as well. When the temperature decreases, plastic shrinks back to its original shape, but the cardboard stays expanded, which causes loosen spool. The spools can be heated up safely up to 45 ºC without this happening.

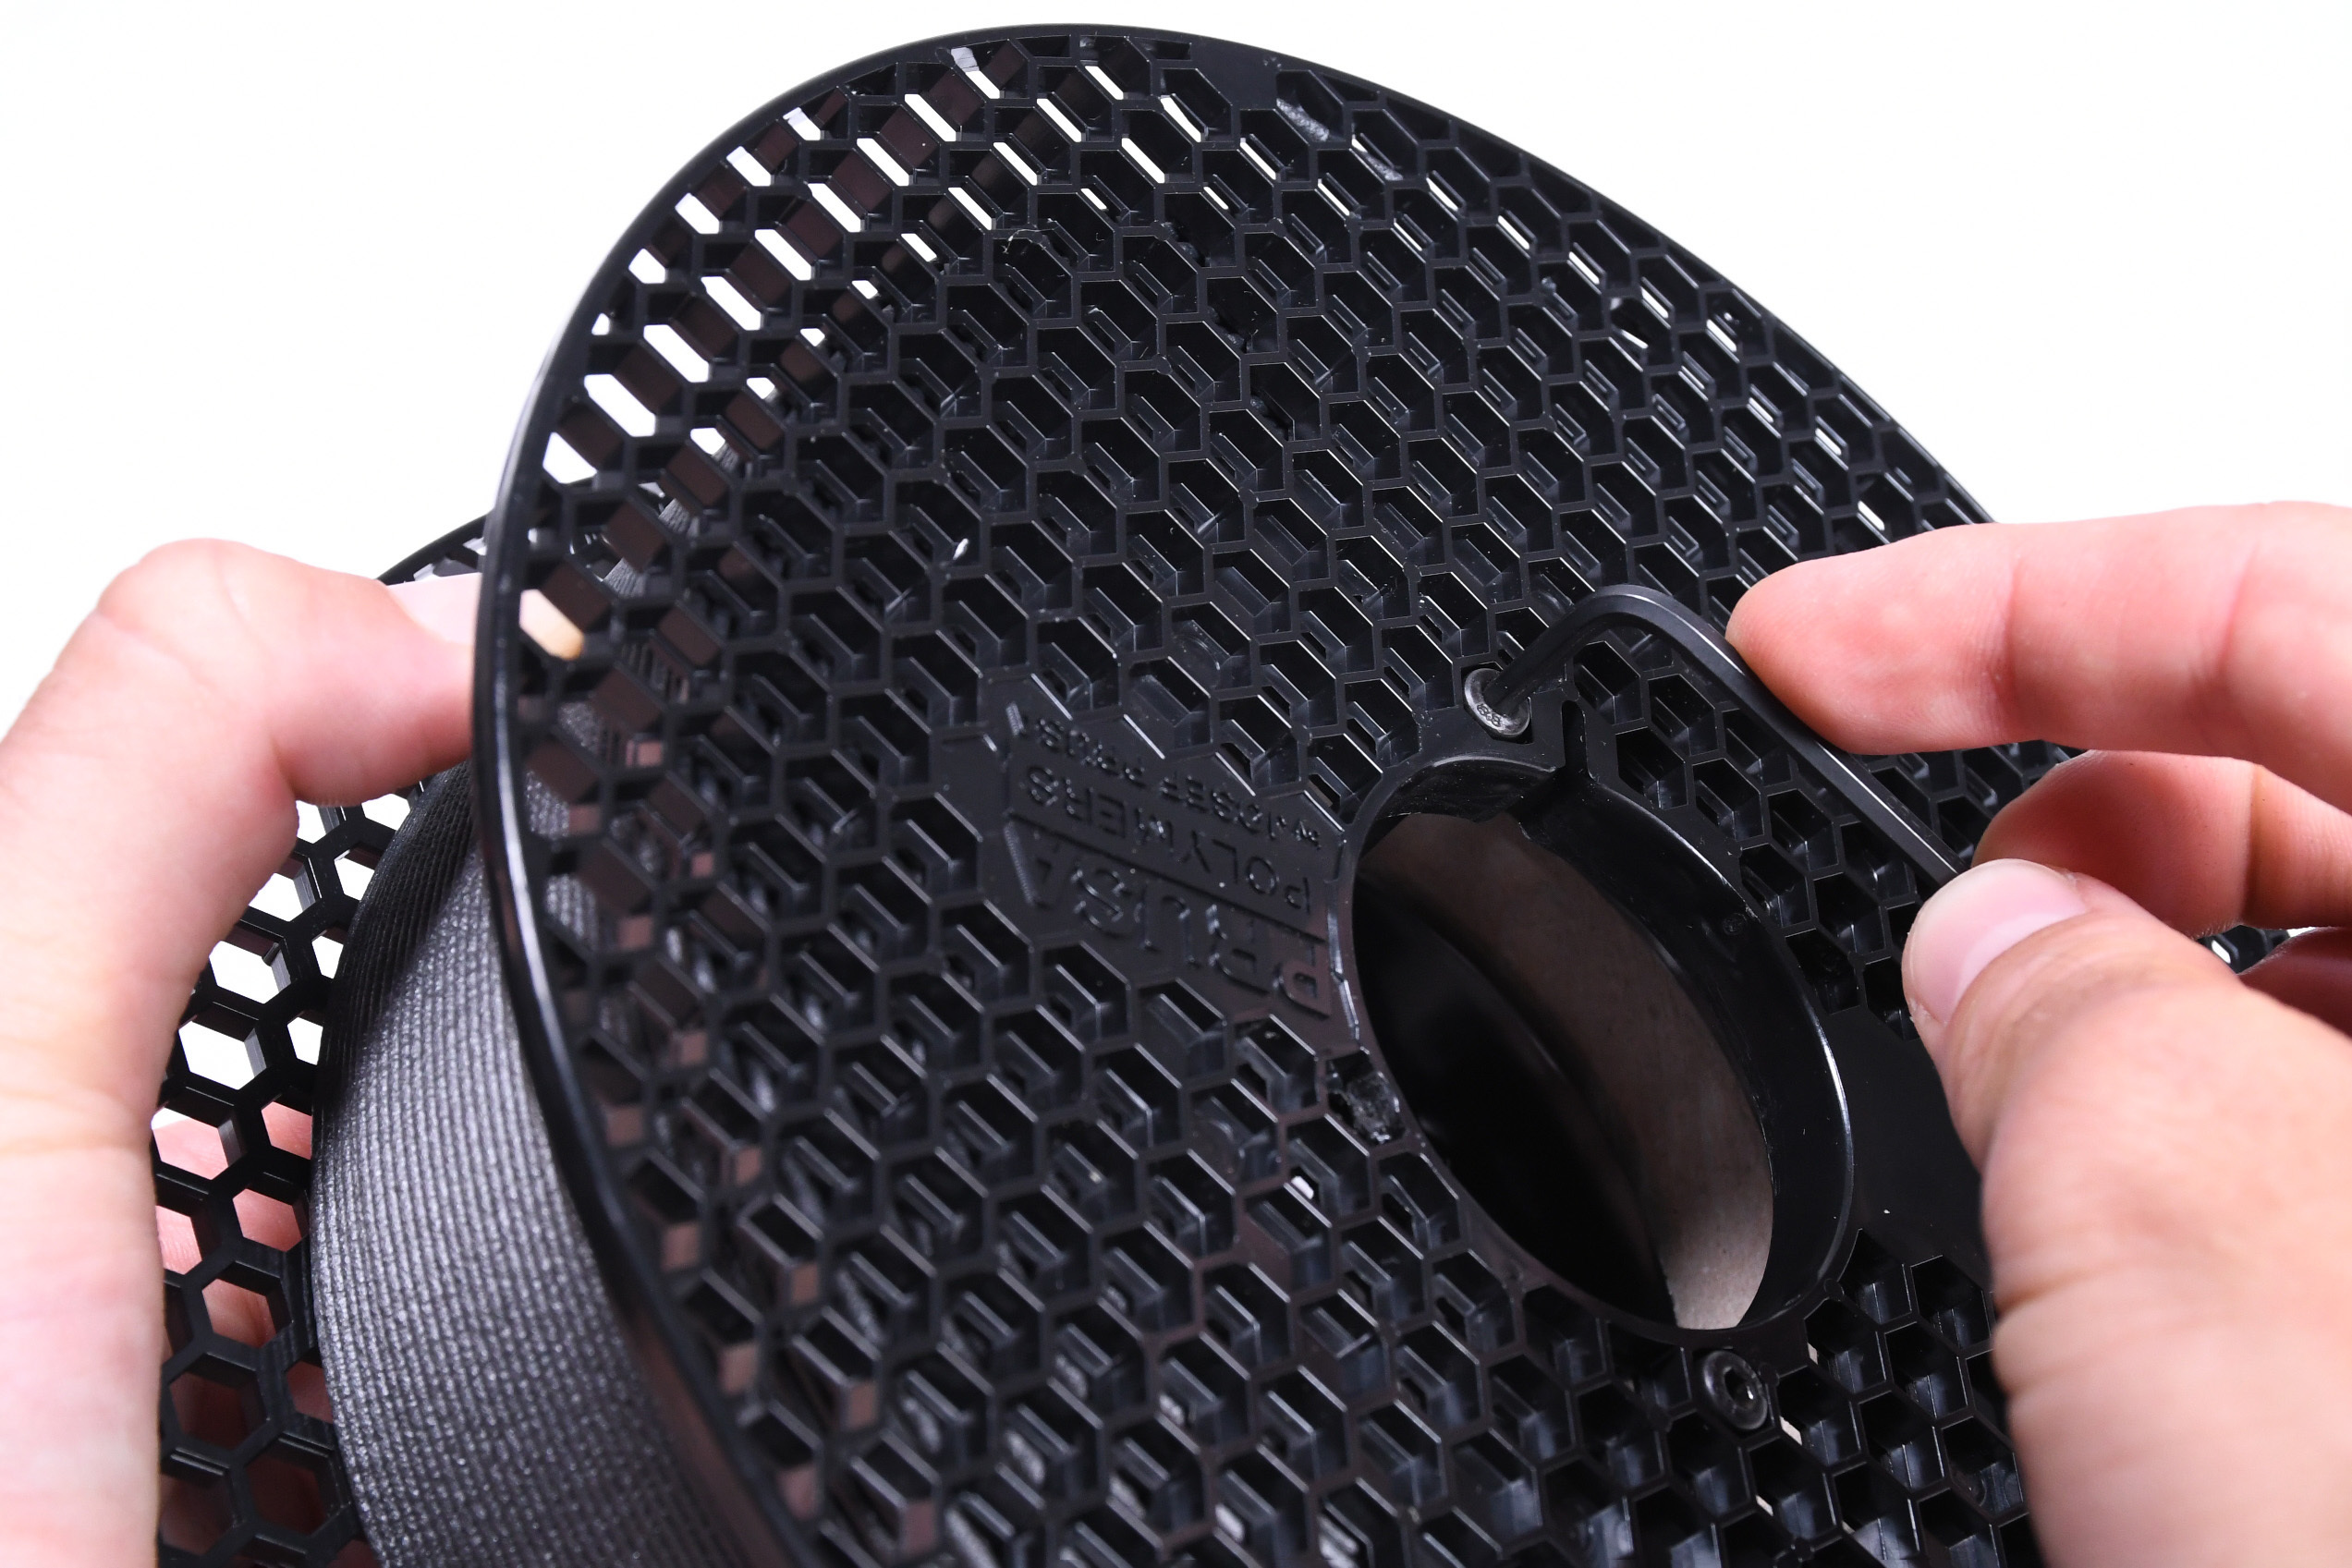
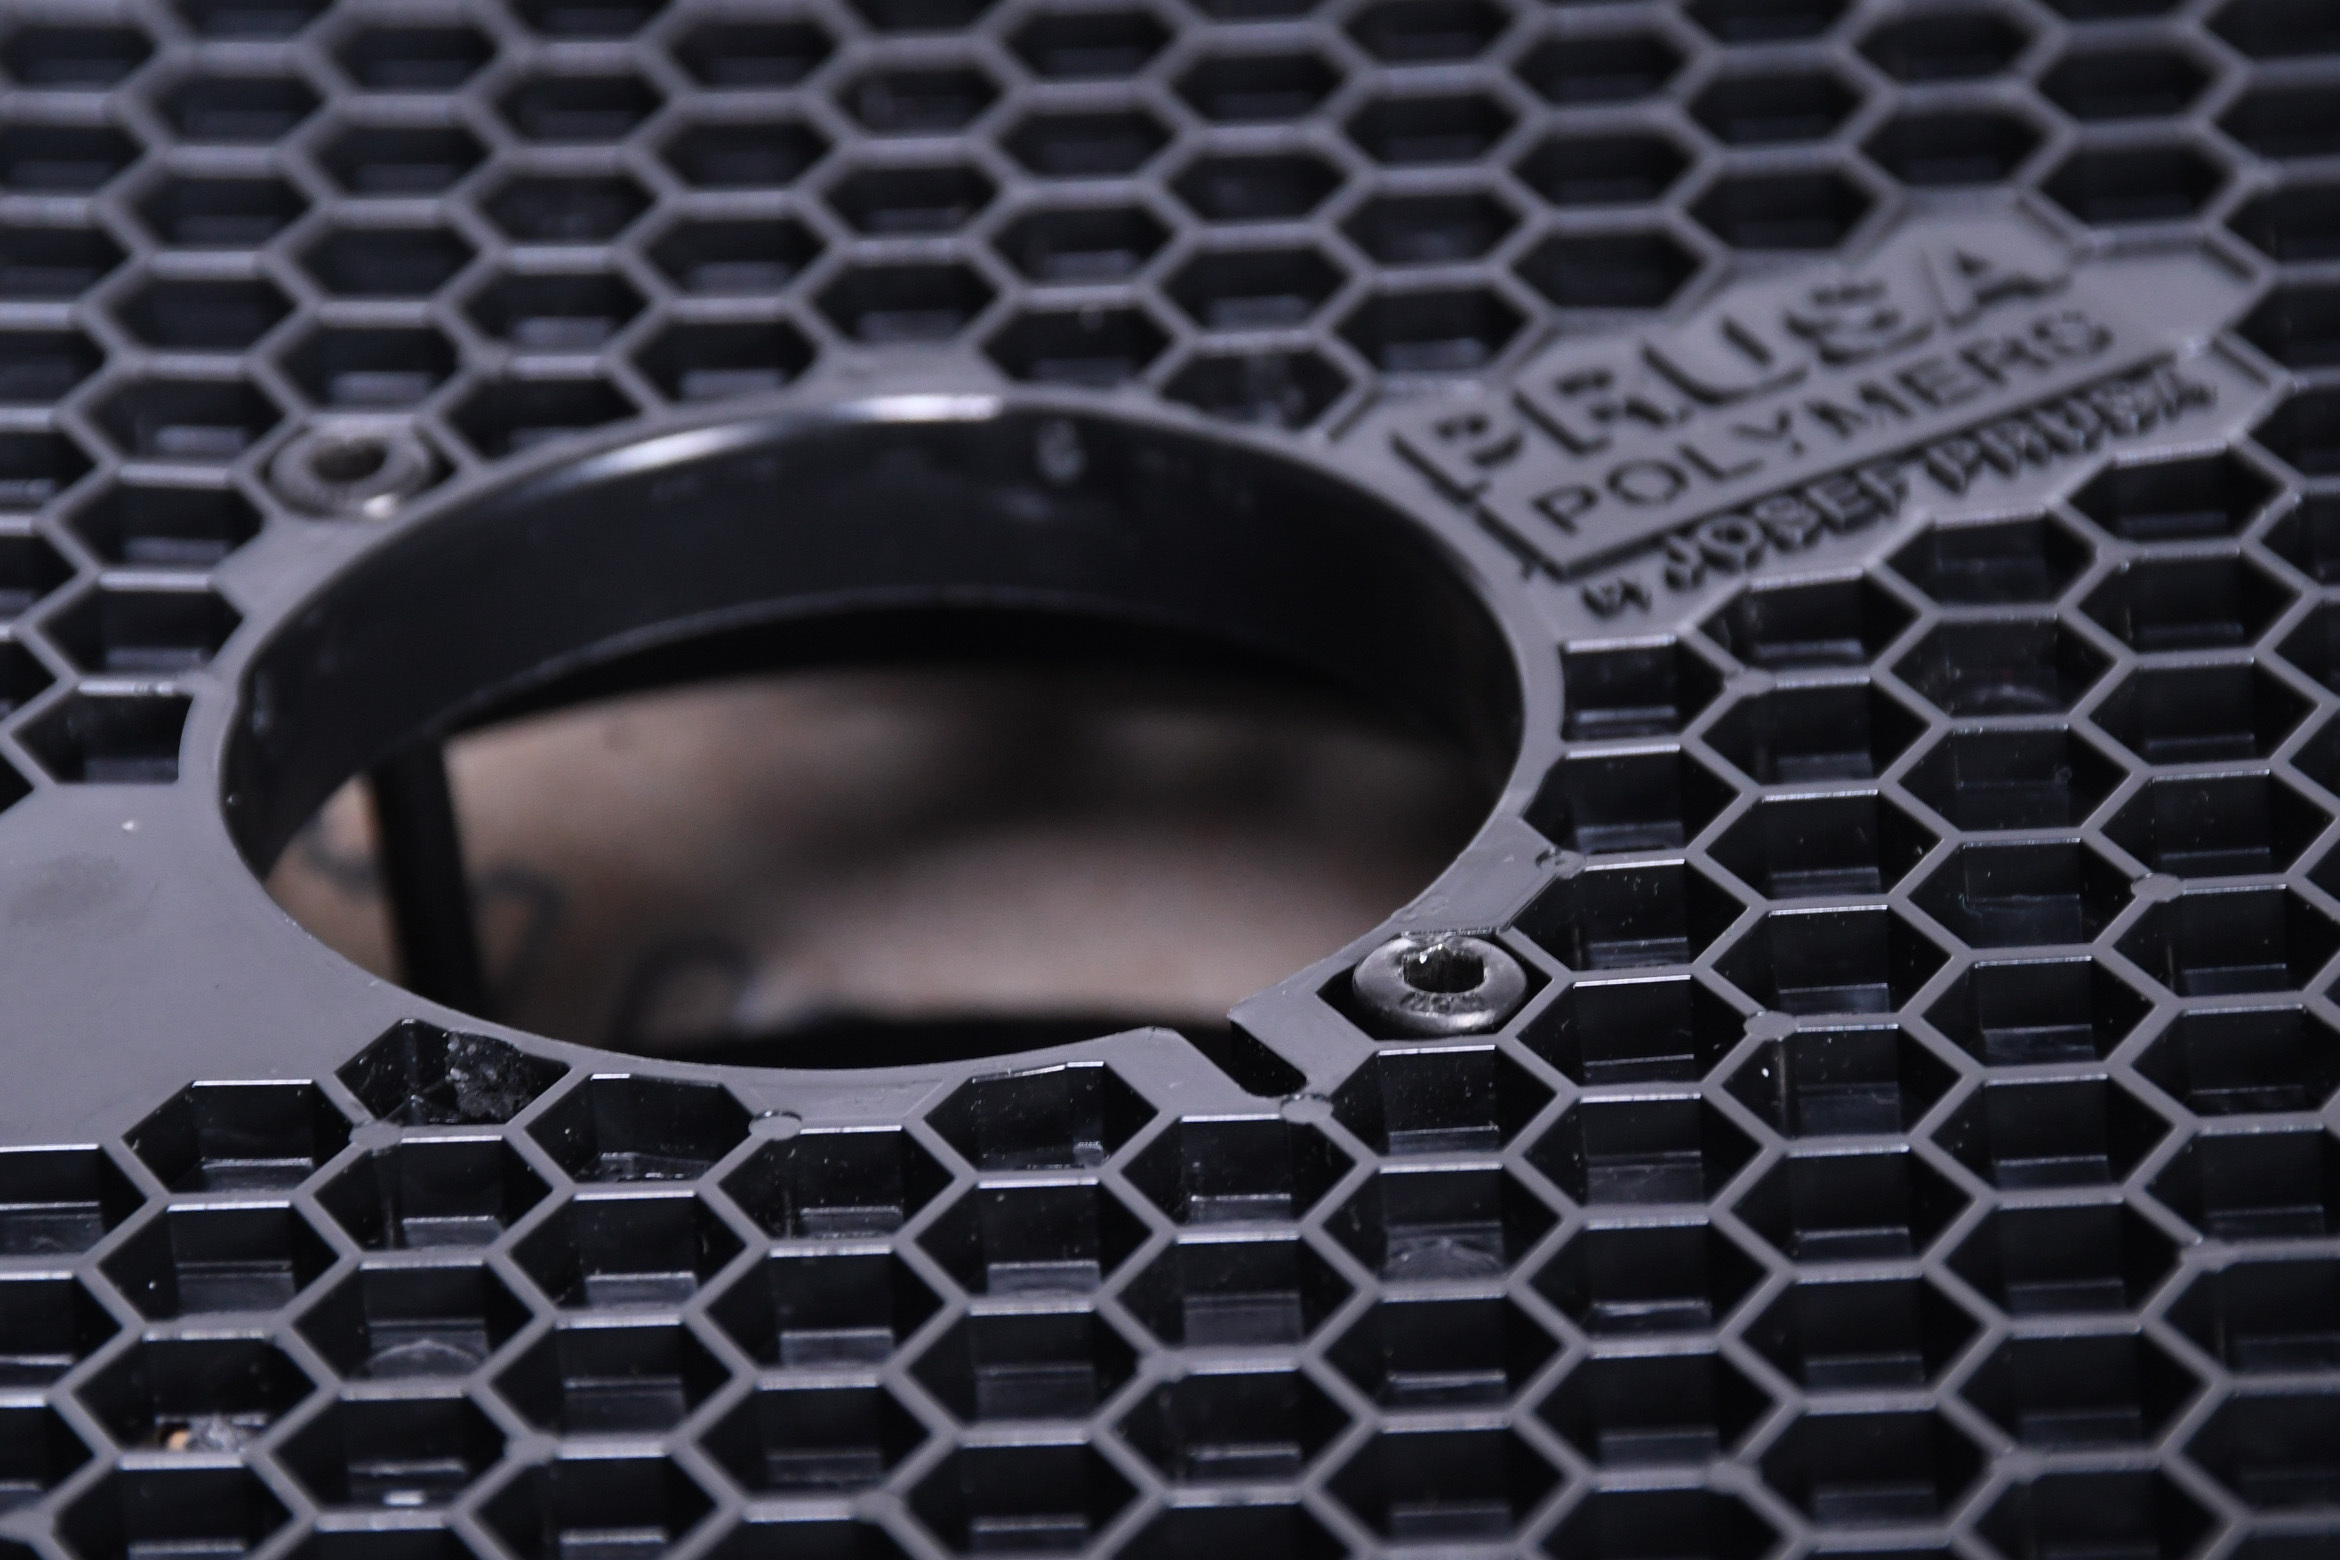
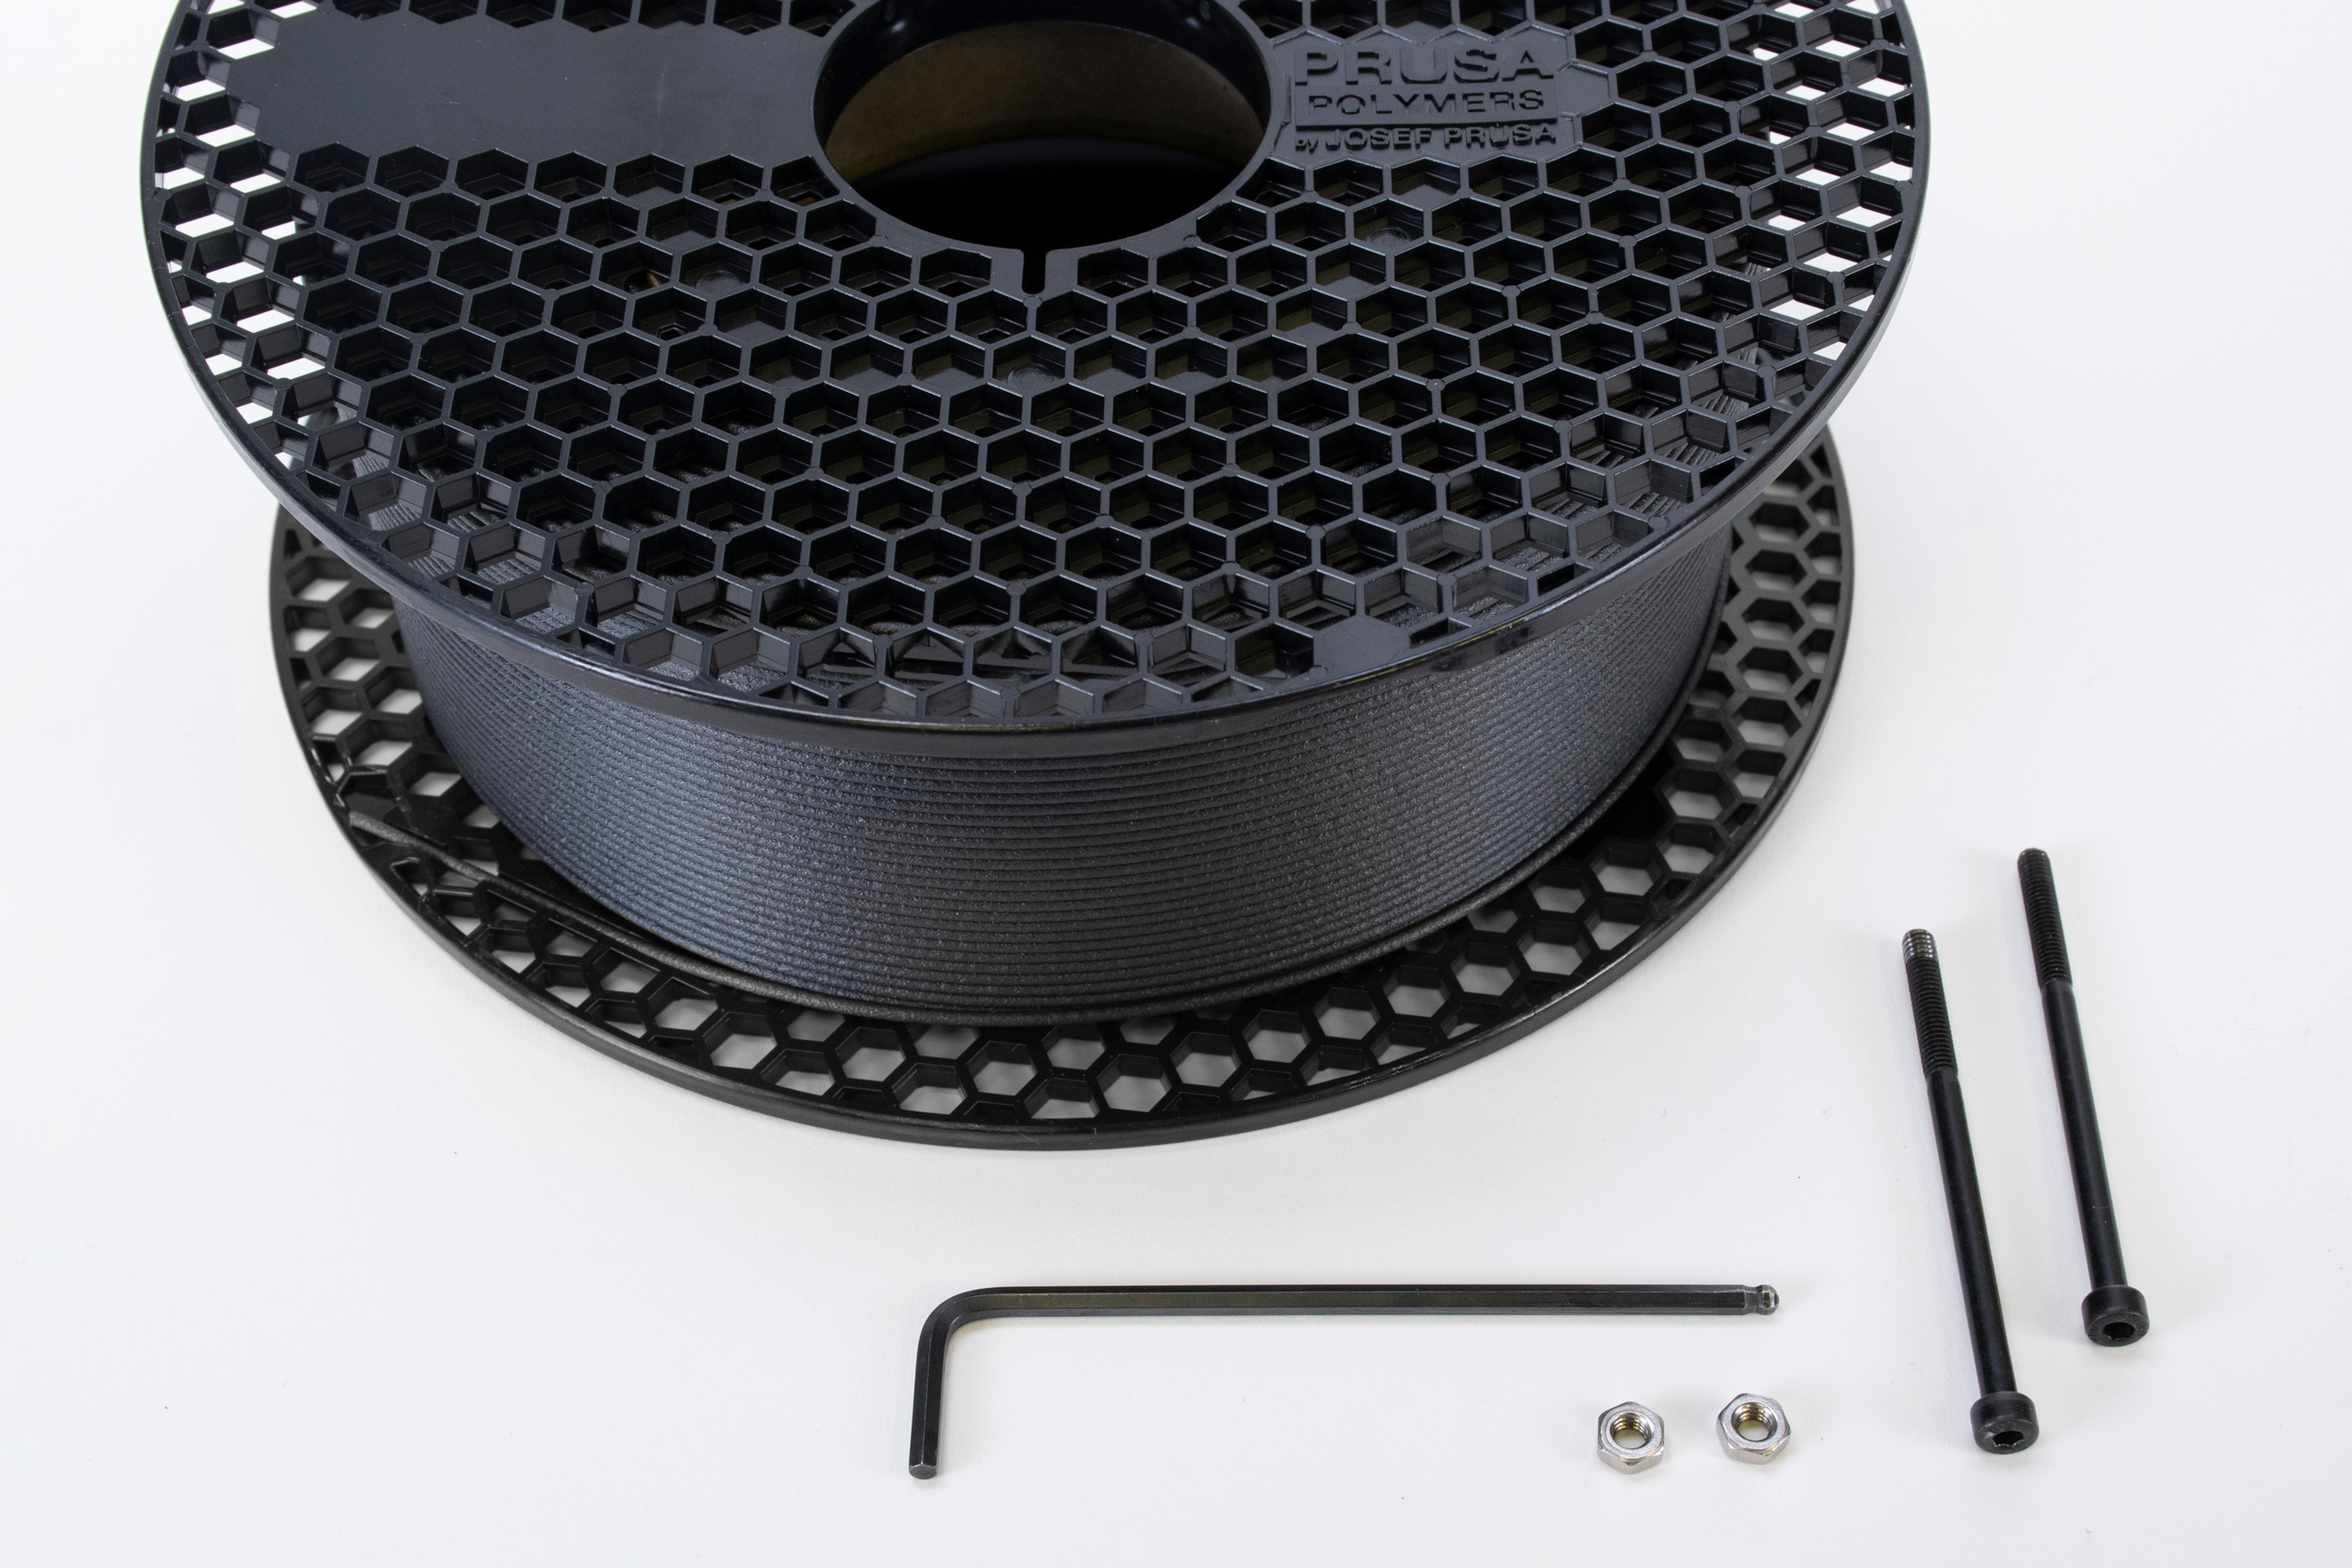
                  Alternatively, it is possible to add a screw holding the two sides of the plastic together. The screw needs to have a thread of at least 65 mm. In the pictures, we use an M4x65 screw, tightened by a 3.5mm Allen key.

                  After heating the spool to above 45 ºC, the screw must hold the spool until the end of its use, or else the spool will fall apart.
                  Prusament Grey spool (old version)

                  The old Prusament spools with grey plastic sides are glued to the cardboard center to prevent falling apart. The glue added can withstand up to 90 ºC. So there is no need to add the screw to dry this spool if this temperature is not exceeded.

                  The old version of PA11CF filament uses the grey Prusament spools. It is recommended to keep this filament in a dry box between each use, even if the filament will be used soon. In case that is not possible, dry the filament before each use.

                  Drying methods

                  Temperatures

                  Once you are sure that the spool will not fall apart, the following temperatures and times are recommended for the Prusament materials. It is important not to exceed these temperatures while drying the filament, or the filament will soften and stick together.

                  Also, it is important to stick to the recommended drying times to prevent overdrying.

                  MaterialTemperatureTime
                  PLA/rPLA45 ºC6 hours
                  Woodfill45 °C6 hours
                  PVB45 ºC8 hours
                  PETG (all versions)55 ºC6 hours
                  TPU60 °C4-6 hours
                  PP Carbon Fiber/Glass Fiber70 °C2-4 hours
                  ASA80 ºC4 hours
                  PC Blend85 ºC5 hours
                  PC Blend Carbon Fiber90 ºC4 hours
                  PC Space Grade90 °C4-6 hours
                  PA11 Carbon Fiber90 ºC6 hours
                  PEI150 °C8 hours

                  Filament dryer

                  There are specialized boxes that will not only keep filaments dry but also actively remove the moisture from filaments. Usually, you are also able to keep the filament in the box while printing.

                  Make sure to check the specifications of the box you intend to use to make sure that it matches the drying temperature of your filament.

                  To maintain low humidity during printing, we recommend using the Prusa Pro Filament Drybox or Prusa USS Drybox.

                  Oven

                  Since most people have an oven at home, this seems the easiest way to dry filament. However, some things need to be noted for filament drying in a conventional oven.

                  Home ovens don't have a very precise temperature measurement. The fluctuations that do not affect your food might damage your filament, especially low-temperature ones like PLA. If using an oven, make sure to have an external thermometer to correct the temperature if necessary.

                  Another issue is that a lot of home ovens cannot be set at a temperature low enough to dry the filaments without damaging them. Even if left for less time than recommended, high temperatures will damage the filament.

                  Professional drying ovens

                  If you need to dry high-performance or highly hygroscopic materials (such as PEI, PEEK, or carbon-filled nylons) with precise and stable temperature control, we offer laboratory-grade drying ovens.

                  We offer the Memmert UF-series ovens, which feature accurate temperature regulation, adjustable fan speed, and exhaust flap settings suitable for advanced filament drying.

                  For more information about setup and drying workflow, see Drying filament in Memmert UF-series universal oven.

                  Food dehydrator

                  A different method of drying is adapting a food dehydrator to fit a filament spool inside. The adaptation is usually achieved by taking off the trays between the layers and placing the filaments inside. These dehydrators usually have only low temperatures, so check the drying temperature of your filament before purchasing one.

                  After drying, make sure to store the filament properly.
                  Was this article helpful?
                  This action is available only to registered users. Please log-in.

                  Topics

                  • Using the printer
                    • Material guide
                      • ASA
                      • Flexible materials
                      • ABS
                      • PETG
                      • PLA
                      • Polycarbonate (PC)
                      • Composite materials (with metal or wood particles)
                      • CPE
                      • Water soluble (BVOH/PVA)
                      • HIPS
                      • Polypropylene (PP)
                      • NGEN
                      • Polyamide (Nylon)
                      • Composite materials (filled with carbon, kevlar or glass)
                      • PVB
                      • LW PLA
                      • Drying filament
                      • How to use Prusament refill 1kg
                      • PEI (Ultem)
                      • HueForge filament transparency values and HexCodes
                      • PEEK-CF (Polyetheretherketone)
                      • PEKK-CF (Polyetherketoneketone)
                      • PPS (Polyphenylene sulfide)
                      • PSU (Polysulfone)
                      • PPSU (Polyphenylsulfone)
                      • How to print with PEI 1010
                      • Prusament TPU 95A material guide
                      • Prusament PETG Ultraglow troubleshooting
                      • Prusament Woodfill
                      • PETG V0
                      • PETG Magnetite 40%
                      • PETG Tungsten
                    • 3D models
                    • Slicing
                    • Printer maintenance
                    • Prusa Connect & PrusaLink

                  19 comments

                  Log in  to post a comment
                  James Ramsey
                  •
                  What happens if Prusament PC-CF is dried at 85°C instead of 90°C? There are far more filament dryers that reach the former temperature than the latter.
                  Reply
                  Makubuya Festo
                  •
                  Kindly update info on the new spools with NFC
                  Reply
                  Iustin Pop
                  •
                  The information here is out of date for the new NFC-enabled spools. From the blog post that introduced them, quote:

                  "We replaced the original paper core with a plastic one equipped with a locking mechanism, and we manufacture the whole spools from recycled polycarbonate. This ensures high reliability at temperatures up to 100 °C. And the High-Temp spools we use for PEI resist up to 150 °C, even with the OpenPrintTag inside."

                  Would be good to update the article!
                  Reply
                  Preston L. Bannister
                  •
                  First, there is a lot of chemical energy in a roll of filament, so an oven with wide temperature swings might risk a rather dramatic fire (i.e. chance of burning down your house!). Best to put an accurate thermometer in oven, and check the temperature. Also watch carefully, at least the first time you do this.

                  That said, I have a slightly-fancy countertop convection oven (Breville) that seems to have very well-regulated temperature. Drying PLA at 130°F for an hour (the fan moving air in the oven) seems to do the trick for me. (Not done anything empirical.) With PLA ~60-65°C (140-149°F) is the glass transition temperature, so we are well below.

                  (CNC Kitchen did a video on this, a while back.)
                  Reply
                  bbum
                  •
                  The drying times are way too long. No harm done but wasted time and energy.

                  TPU? 90 minutes, typically.
                  PLA/PETG? 60-90 minutes.

                  Now, obviously, the relative humidity in the surrounding environment will be a major factor. Your drying times might be longer. (Also funny to note that most sites say TPU requires 8 hours @ 50-60).
                  Reply
                  Jan Novák
                  •
                  Thank you for your suggestion. Drying depends on many factors, including the number of filament layers on the spool, air permeability to the bottom layers, and others. The listed values are based on our long-term testing.
                  Reply