Prusa
  • ショップ
    • 最新製品
    カテゴリー別
    • 3Dプリンター新着
    • 3Dプリンターアップグレード新着
    • 材料
    • アクセサリー
    • スペアパーツ
    • コース
    • グッズ
    • 見積もりを取得
    クイックリンク
    • 配送と配達
    • 返品と返金
    • 支払いと融資
    • 保証
    • VATと関税
    • よくある質問

    0 点の商品がカートに入っています点の商品がカートに入っています

    カートは空です

    カートを見る3Dプリンターを購入

    マイプロフィール

    ログイン すると注文や保存した商品を確認できます

    マイプロフィール

    ログイン中:

    • 注文
    • ログアウト
  • 3Dプリント
    • 3Dプリントを探る
    初心者向け
    • 3Dプリントの基礎
    • FDM印刷の仕組み
    • 初めてのプリンターを購入する
    • 3Dモデルカタログ
    用途別
    • ラピッドプロトタイピング
    • 製造
    • エンジニアリング
    • 研究
    • アートとデザイン
    さらに深く
    • 材料ガイド
    • コース
    • ウェビナー
    • 導入事例
    • カスタム3Dプリンティング
  • 3Dプリンター
    • すべての3Dプリンター
    用途
    • 自宅またはガレージ愛好家、改造愛好家、ホームプリンティング
    • ビジネス小規模チーム向けの社内生産
    • エンタープライズフリート、セキュリティ、大規模生産
    • どのPrusaが私に適していますか
    ショップと閲覧
    • CORE One+新着
    • CORE One+ INDX新着
    • CORE One L+新着
    • CORE One L+ INDX新着
    • XL+新着
    • MK4S
    • Prusa Pro HT90
    • Prusa Pro AFS
    • Prusa Pro SLX
    プリンターからさらに
    • 部品とアップグレード新着
    • Spare parts
    • 重要インフラ
    • 導入事例
    • シグネチャーオーク
    • キット
  • 材料
    • すべての材料
    用途別
    • 日常とデザイン
    • 機能工学
    • 複合材料
    • プロフェッショナル向け特殊材料
    • SLAレジン
    Prusament
    • PLA
    • PETG
    • ASA
    • PC
    • PA11
    • Flex
    • TPU
    材料からさらに
    • 材料ガイド
    • 自社製材料
    • サステナビリティ
    • ストアで注文
  • ソフトウェア
    • すべてのソフトウェア
    印刷の準備
    • PrusaSlicer 3.0新着
    印刷と監視
    • Prusa Connect
    • EasyPrint
    • iOS & Androidアプリ
    • Prusaファーム
    始める
    • ダウンロードとインストール
    • ナレッジベース
    その他のソフトウェア
    • 3Dモデルカタログ
  • サポート
    • サポートを探す
    回答を探す
    • ナレッジベース
    • トラブルシューティング
    • コース
    • ウェビナー
    ヘルプ
    • お問い合わせ
    • ライブチャット
    • 配送と配達
    • 保証
    • 返品と返金
    • サービスとスペアパーツ
    • サービスと修理
    コミュニティ
    • フォーラム
    • Reddit
    • Printables
  • トラストセンター
    • トラストセンター概要
    トピック別
    • GDPR
    • 証明書
    • セキュリティ
    • コンプライアンス
    コミットメント
    • サステナビリティレポート
    お問い合わせ
    • セキュリティチームに連絡
  • 会社
    • Prusaについて
    私たちについて
    • 私たちのストーリー
    • プリンターの製造方法
    • オープンソース
    • ブランド&メディアキット
    ニュース
    • ブログ
    • ニュースルーム
    • イベント
    信頼とパートナー
    • サステナビリティ
    • 再販業者と販売代理店
    • アフィリエイトプログラム
    • お問い合わせ
    • English
    • Čeština
    • Deutsch
    • Español
    • Français
    • Italiano
    • Polski
    • 日本語
  • ログイン中:

    • 注文
    • 住所
    • 在庫アラート
    • マイコース
    • サブスクリプション
    • アカウントを編集
    • ログアウト

ログイン すると注文や保存した商品を確認できます

ログイン中:
  • 注文
  • 住所
  • 在庫アラート
  • マイコース
  • サブスクリプション
  • アカウントを編集
  • English
  • Čeština
  • Deutsch
  • Español
  • Français
  • Italiano
  • Polski
  • 日本語
ショップ

0 点の商品がカートに入っています点の商品がカートに入っています

カートは空です

カートを見る3Dプリンターを購入

マイプロフィール

ログイン すると注文や保存した商品を確認できます

マイプロフィール

ログイン中:

  • 注文
  • ログアウト
ショップ
  • 最新製品
カテゴリー別
  • 3Dプリンター新着
  • 3Dプリンターアップグレード新着
  • 材料
  • アクセサリー
  • スペアパーツ
  • コース
  • グッズ
  • 見積もりを取得
クイックリンク
  • 配送と配達
  • 返品と返金
  • 支払いと融資
  • 保証
  • VATと関税
  • よくある質問

おすすめ製品

    人気のカテゴリー

      急上昇ワード

        記事

          ブログ

            製品

              カテゴリー

                検索候補

                  検索中…
                  結果がありません
                  エラーが発生しました。
                  ↑↓ 選択↵ 開くEsc 検索を閉じる
                  1. サポート
                  2. プリンタートラブルシューティング
                  3. Selftest failed (CORE One INDX)
                   

                  内容

                  • Calibrations & Tests
                  • Door sensor
                  • X and Y axes test
                  • Z alignment calibration
                  • Belt tuning
                  • Homing calibration
                  • Dock calibration
                  • Loadcell test
                  • Z axis test
                  • Fan test
                  • Heater test
                  • Tool offset calibration
                  • Nozzle cleaner calibration
                  • Filament sensor calibration
                  • Phase stepping calibration
                  • Input shaper calibration

                  ブログ

                  • Prusament PLA ColorMix:わずか5巻のフィラメントで45色以上をプリント
                  • PrusaSlicer 3.0プレビュー版 — 3Dプリントの未来を見据えた仕様
                  • より高品質なプリントを、もっと簡単に:Prusa XL+、CORE One L+、CORE One+(Gen 2)― 大規模製品アップグレード

                  ニュースレター

                  ご登録いただくと、毎月 新しいファームウェア、PrusaSlicerの新バージョン、3Dプリントプロジェクトの一般的なヒントなど、役立つ情報をお届けします。

                  クリックして、ニュースレターを受け取る。

                  このサイトはreCAPTCHA Enterpriseによって保護されており、Googleのプライバシーポリシーと利用規約が適用されます。

                  Heavy Duty Keyboard Holder (No Supports)
                  E-shop
                  • 3Dプリンター
                  • プリンターのアップグレード
                  • フィラメント
                  • アクセサリー
                  • Prusa 商品
                  Prusa

                  © Prusa Research a.s.

                  Printables
                  • 3Dモデル
                  • Store
                  • Clubs
                  • 3Dデザインコンテスト
                  • Brands
                  コミュニティ
                  • ワールドマップ
                  • フォーラム
                  • ユーザーグループ
                  • イベント
                  ヘルプ
                  • Prusa ヘルプ
                  • Prusa アカデミー
                  • 3Dプリンティング計算機
                  ソフトウェア
                  • PrusaSlicer
                  • Prusa.app
                  • Prusa Connect
                  • ドライバーとソフトウェア
                  会社概要
                  • 私たちについて
                  • Blog
                  • プルサ正規販売代理店
                  • お問い合わせ
                  • ISO 9001・ISO 14001・ISO 45001 認証取得済み
                  • 一般利用規約
                  • PRUSAウェブサイト利用のための一般利用規約
                  • プライバシーポリシー
                  • クッキーに関する情報
                  • お客様の苦情対応に関する方針
                  • Webサイトのステータスページ
                  • Cookie 設定
                  Prusa
                  • 一般利用規約
                  • PRUSAウェブサイト利用のための一般利用規約
                  • プライバシーポリシー
                  • クッキーに関する情報
                  • お客様の苦情対応に関する方針
                  • Webサイトのステータスページ
                  • Cookie 設定

                  © Prusa Research a.s.

                  JOSEF PRUSA®、PRUSA RESEARCH®、PRUSA POLYMERS®、PRUSA ORANGE®、PRUSA 3D ® および PRUSAMENT® は、Prusa Development a.s. の登録商標であり、Prusa Research a.s. が Prusa Development a.s. からのライセンスに基づき使用しています。

                  Selftest failed

                  (CORE One INDX)

                  関連するもの

                  INDX family
                  記事 他の言語でもご覧になれます。
                  English
                  Čeština
                  Polski
                  Deutsch
                  Français
                  Español
                  Italiano
                  日本語

                  After installing the INDX on your Prusa CORE One/+, the selftest will check the printer's assembly, wiring, and electronic components. It is the first part of the Calibration Wizard, which is prompted automatically when you turn on the printer for the first time or after a factory reset. After the initial calibration is completed, each step of the selftest can be initiated under LCD Menu -> Control -> Calibrations & tests.

                  Note that if the printer is placed on an unstable surface or if another 3D printer is running next to it, it may negatively affect the calibration. The printer should be placed on a stable surface.

                  Remove the top cover for easier access.

                  Calibrations & Tests

                  1. Door sensor
                  2. X axis test
                  3. Y axis test
                  4. Z alignment calibration
                  5. Belt tuning
                  6. Homing calibration
                  7. Dock calibration
                  8. Loadcell test
                  9. Z axis test
                  10. Fan test
                  11. Heater test
                  12. Tool offset calibration
                  13. Nozzle cleaner calibration
                  14. Filament sensor calibration
                  15. Phase stepping calibration
                  16. Input shaper calibration

                  Door sensor

                  If the sensor behaves differently from what is expected in the door sensor calibration, check whether the sensor is working. Go to the LCD menu to Info -> Sensor Info -> Door Sensor. Then, try opening and closing the door and see if the sensor is triggered. If the door does not trigger the sensor, try it by pressing the latch with your finger.

                  If the sensor shows the correct status, go back to the calibration by going to Control -> Calibrations & tests -> Door sensor, and follow the instructions to tighten or loosen the screws.
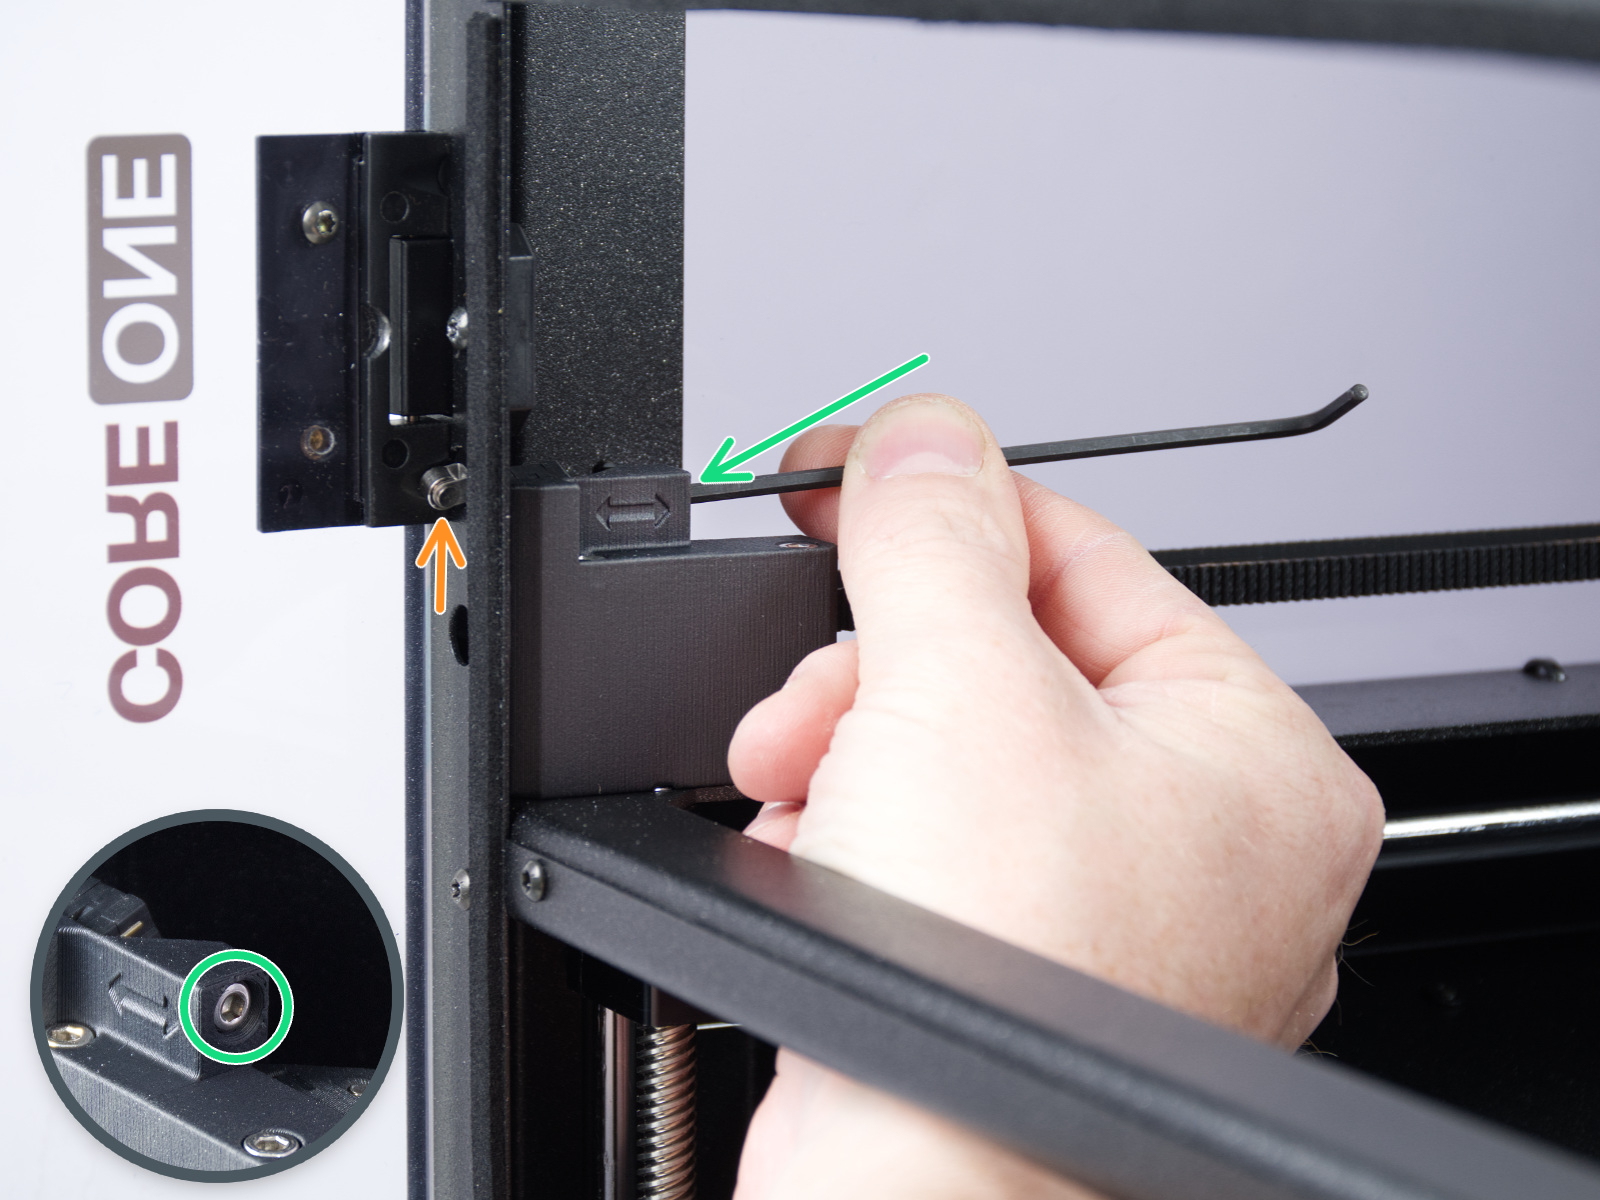
                  On the last part of the calibration, the printer prompts you to place your fingers between the door and the frame. This is meant to prevent injury. If there is an issue with this test, you can keep the door completely open to pass.

                  If the door sensor does not work, check the cable for damage and the connection.

                  X and Y axes test

                  This part of the selftest measures the axis length and motor load.

                  In case of an issue on the X-axis or the Y-axis, make sure that there is no obstacle to the movement, and readjust the belt tension.

                  Also, test the printer movement with the stepper motors temporarily disabled (LCD Menu -> Control -> Disable Motors), moving along both XY diagonals.

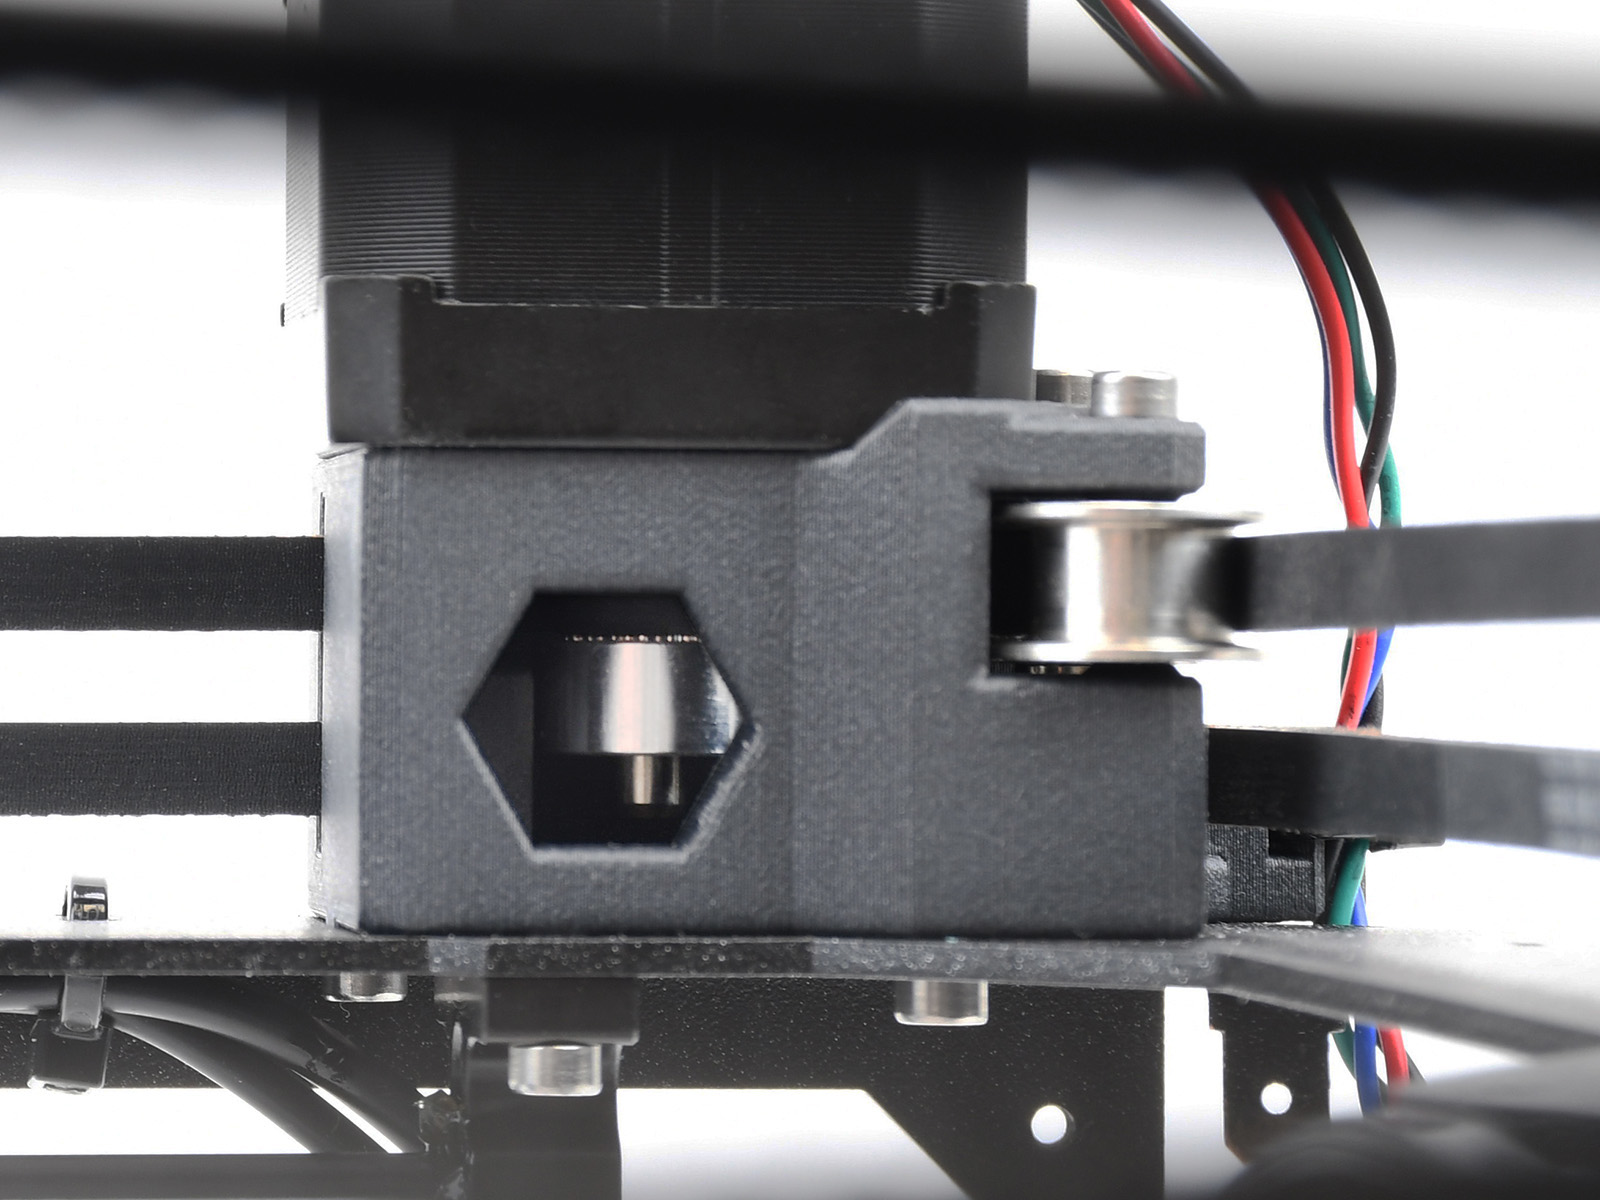
                  If the issue persists, look through the openings on the plastic parts under the CoreXY motors. You will be able to see the motor pulleys. Make sure that they are in the correct orientation, that both set screws are firmly tightened, and that one of them is tightened over the flat part of the motor shaft.
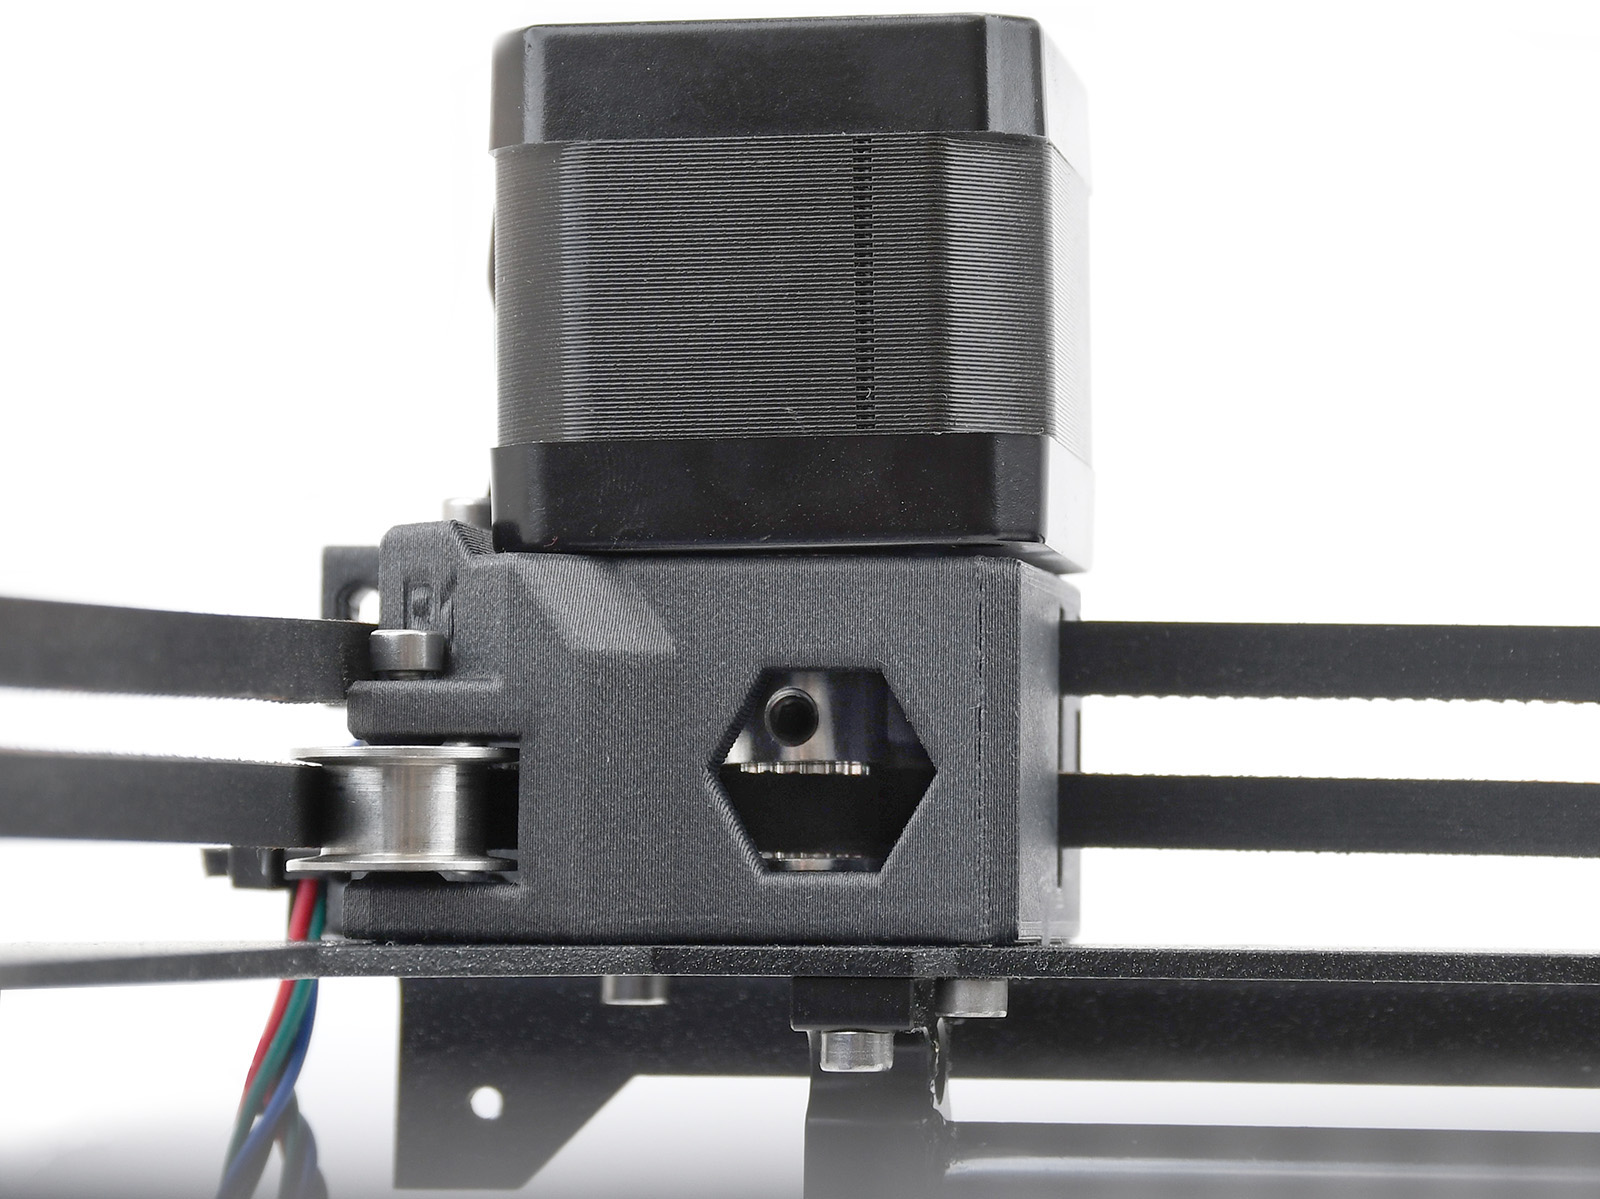
                  Y-motor pulleyX-motor pulley

                  Z alignment calibration

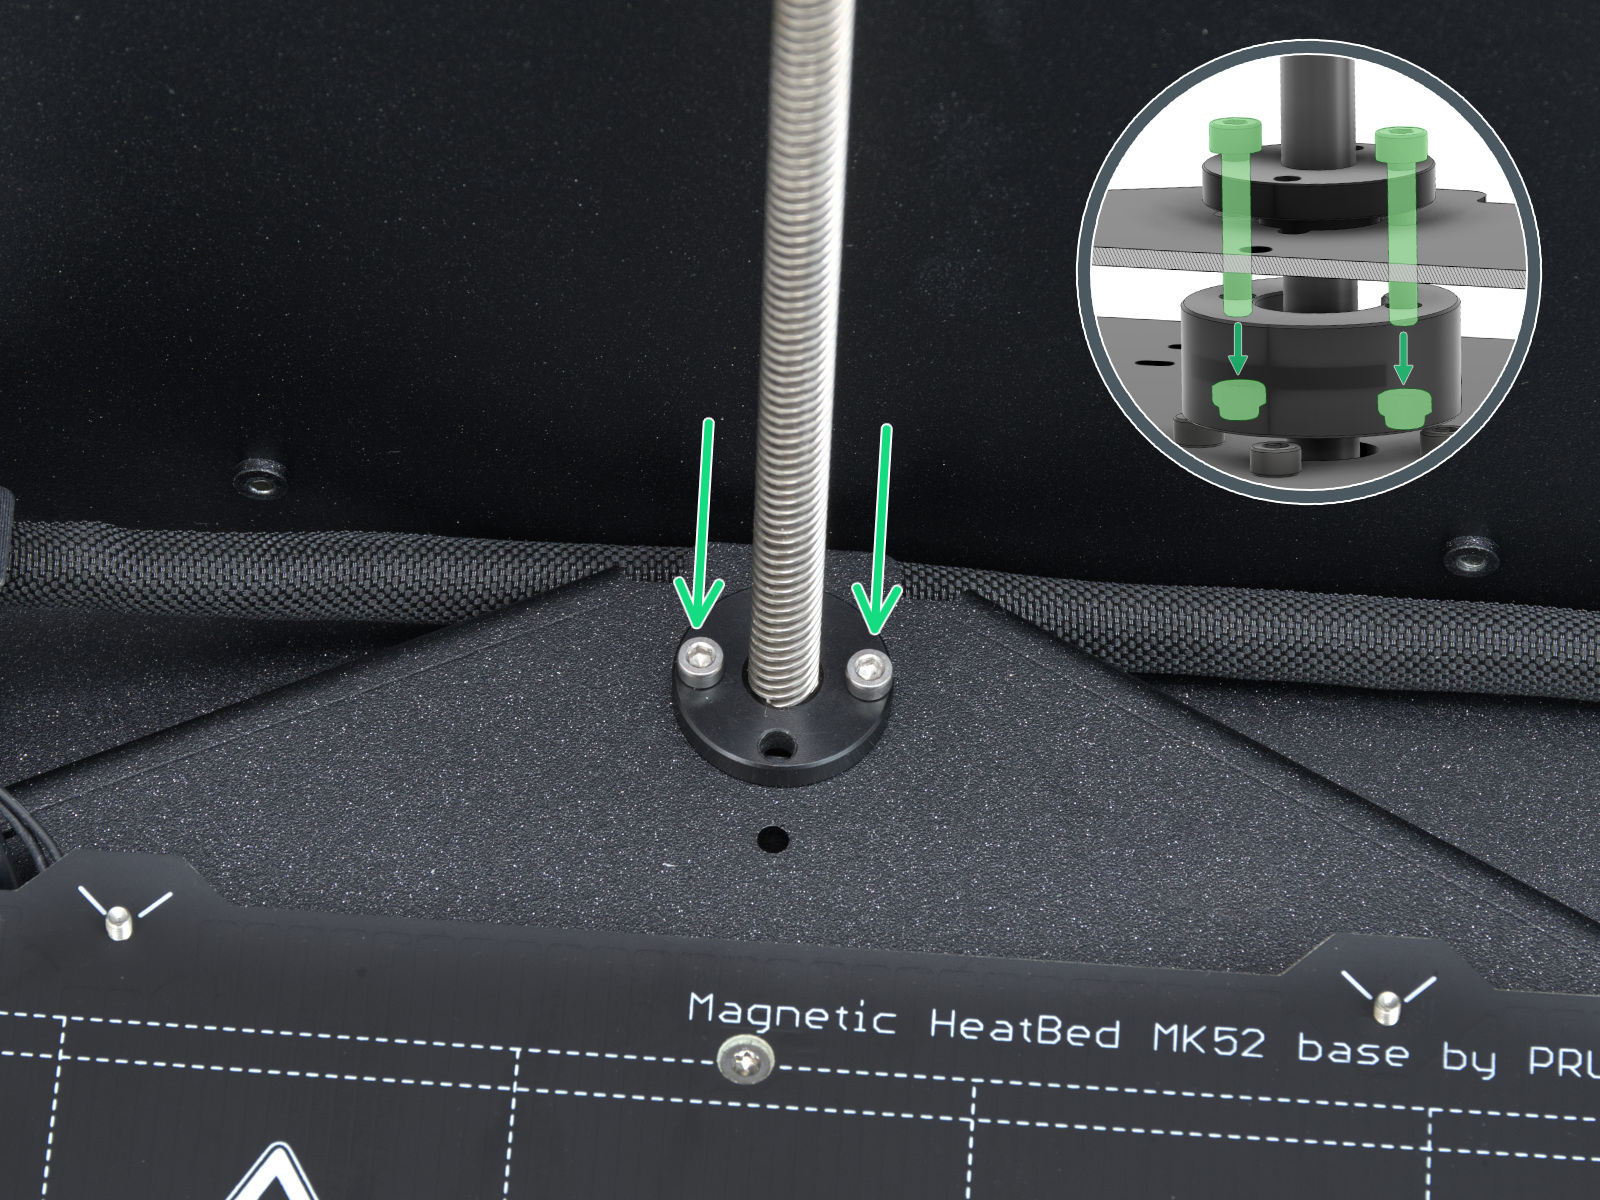
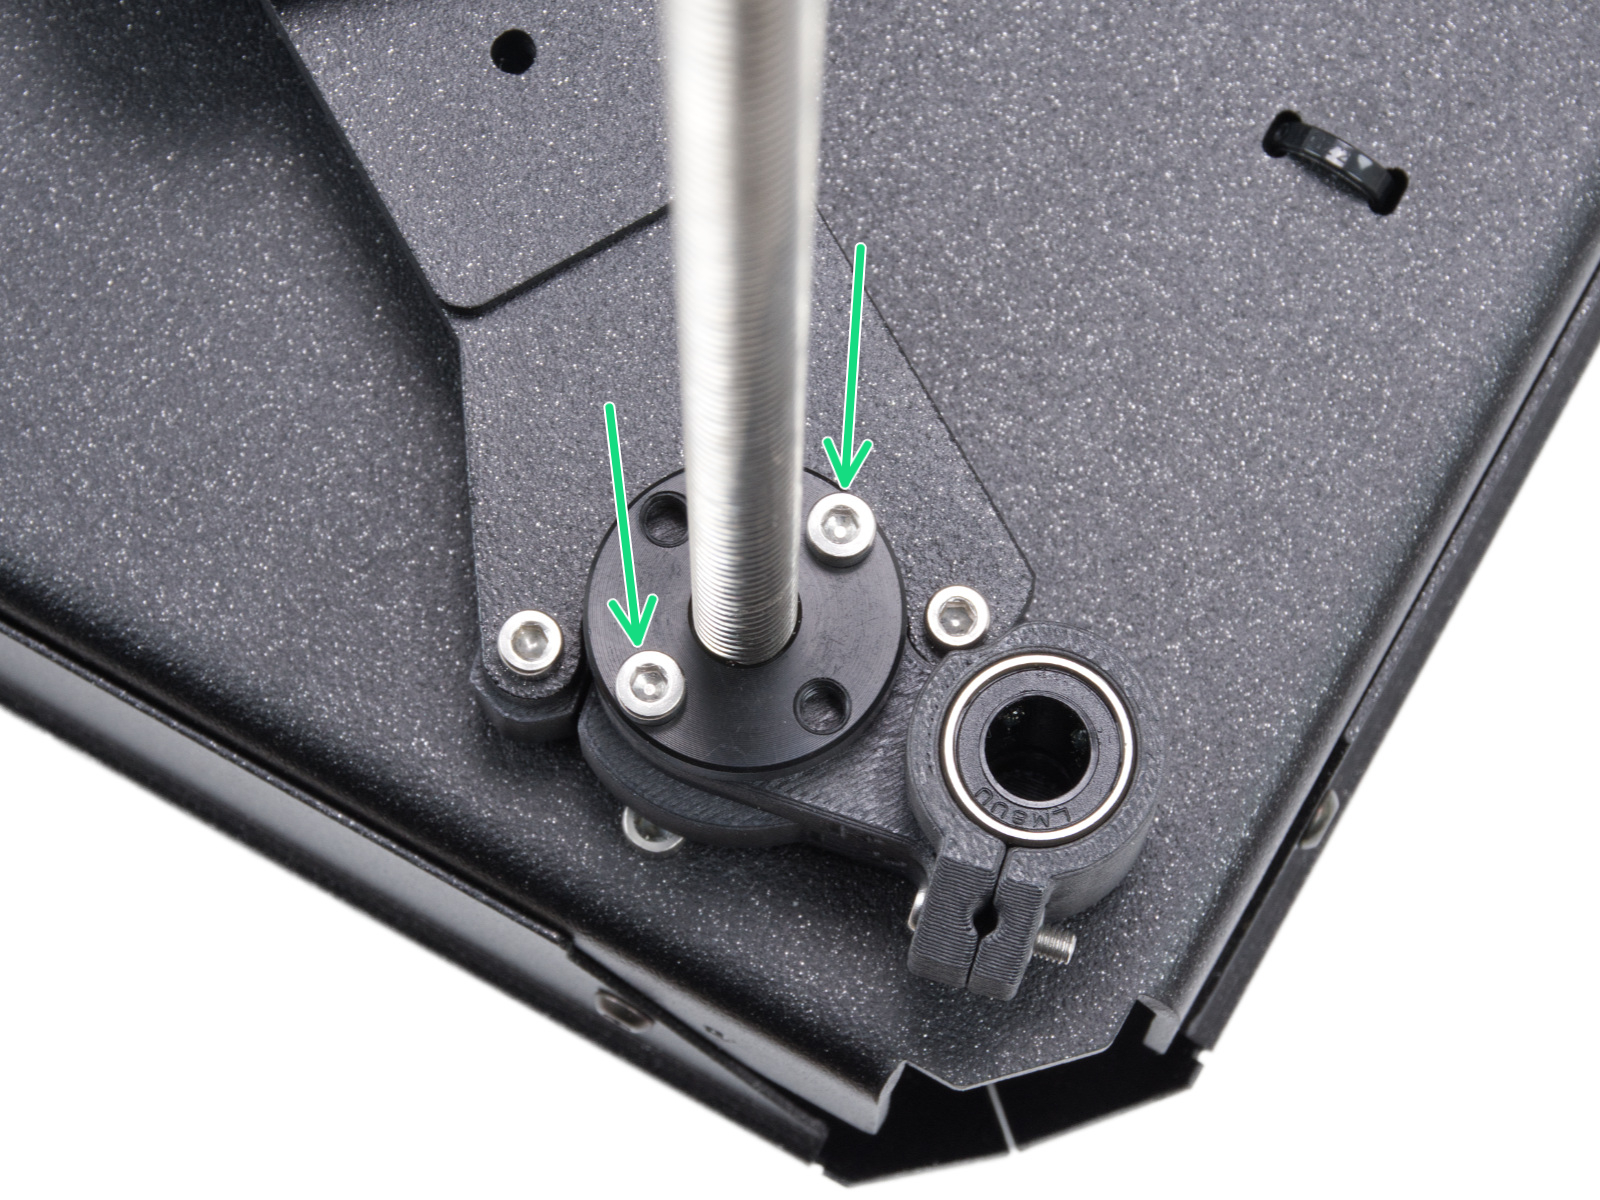
                  This part of the calibration will move to align the three motors on the Z axis so that the heatbed is level. In case of any errors on this test, check the trapezoidal nuts on the motor threaded rods. For that, move the bed all the way down either by the LCD menu in Control -> Move axis -> Move Z, or by turning the threaded rods on the Z motors. Unscrew and remove the screws indicated in the image below. Move the nut along the threaded rod and see if the movement is smooth or not. When the trapezoid nut is still loose, try moving the motor threaded rod by hand (the printer needs to be powered off for that), and see if it turns easily.
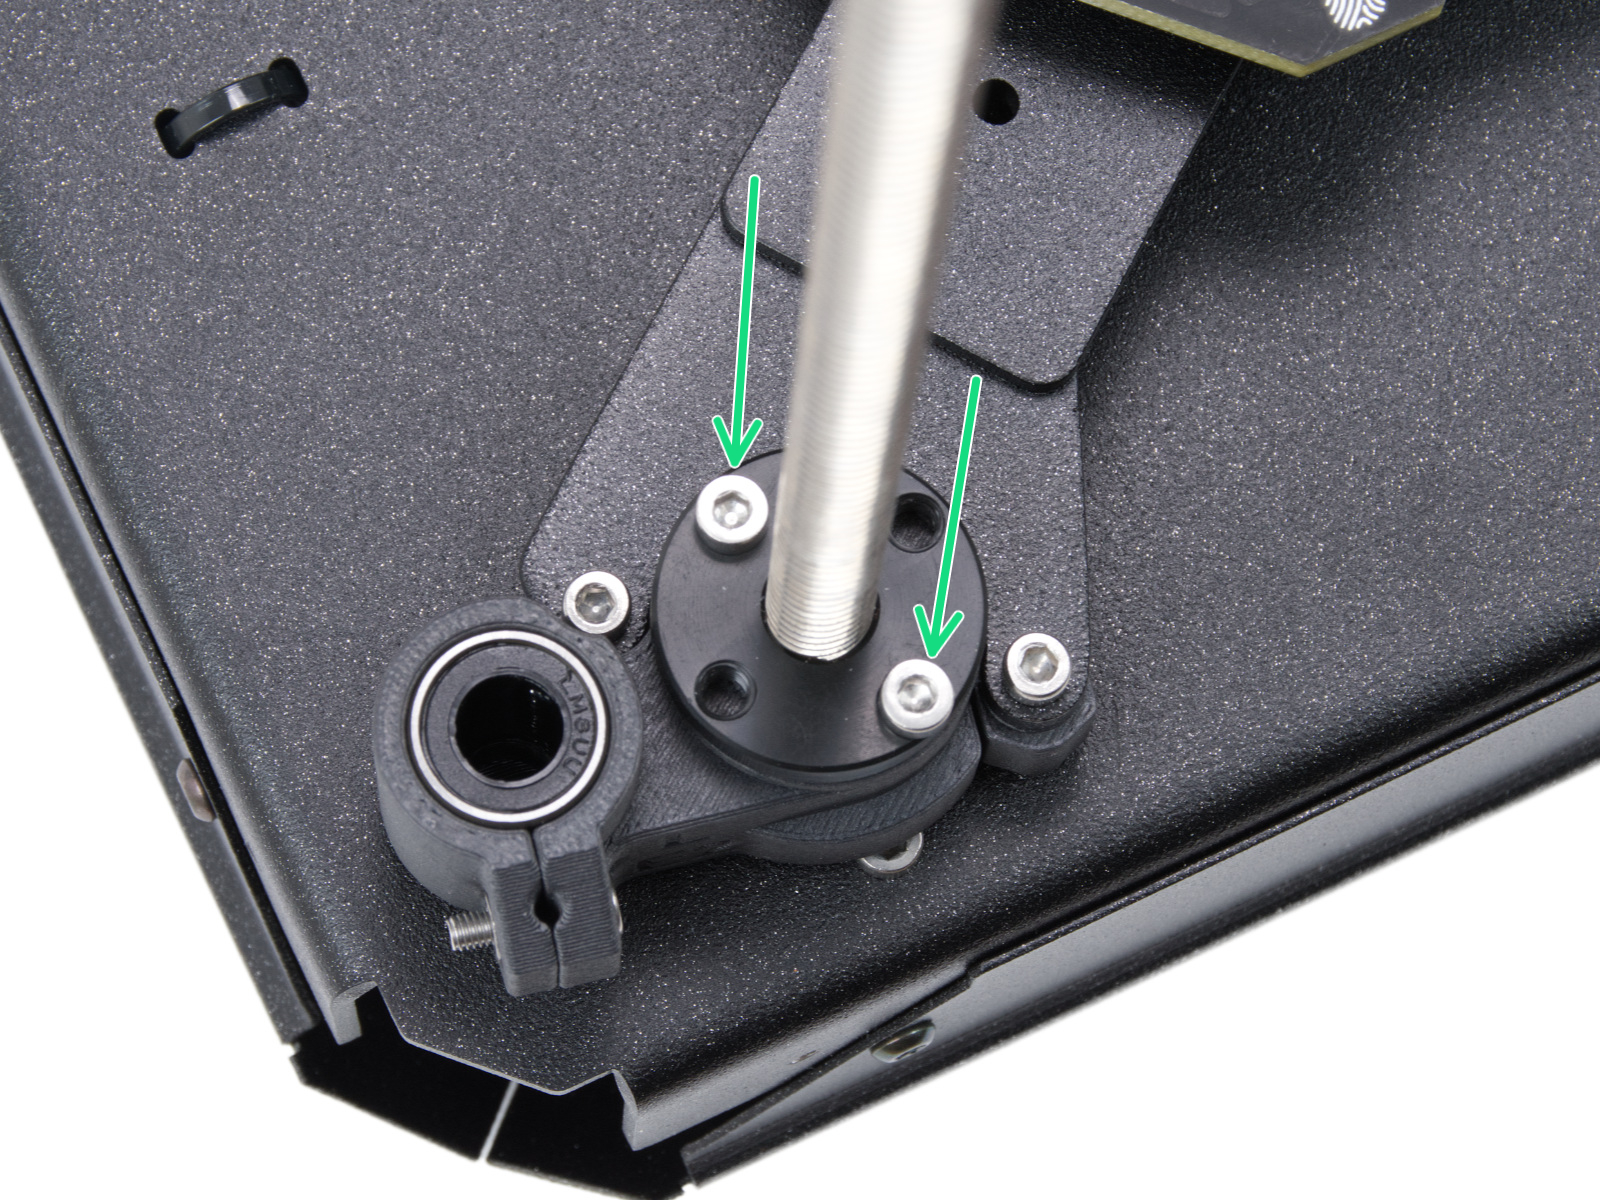
                  Left side trapezoidal nutRear motor trapezoidal nutRight side trapezoidal nut

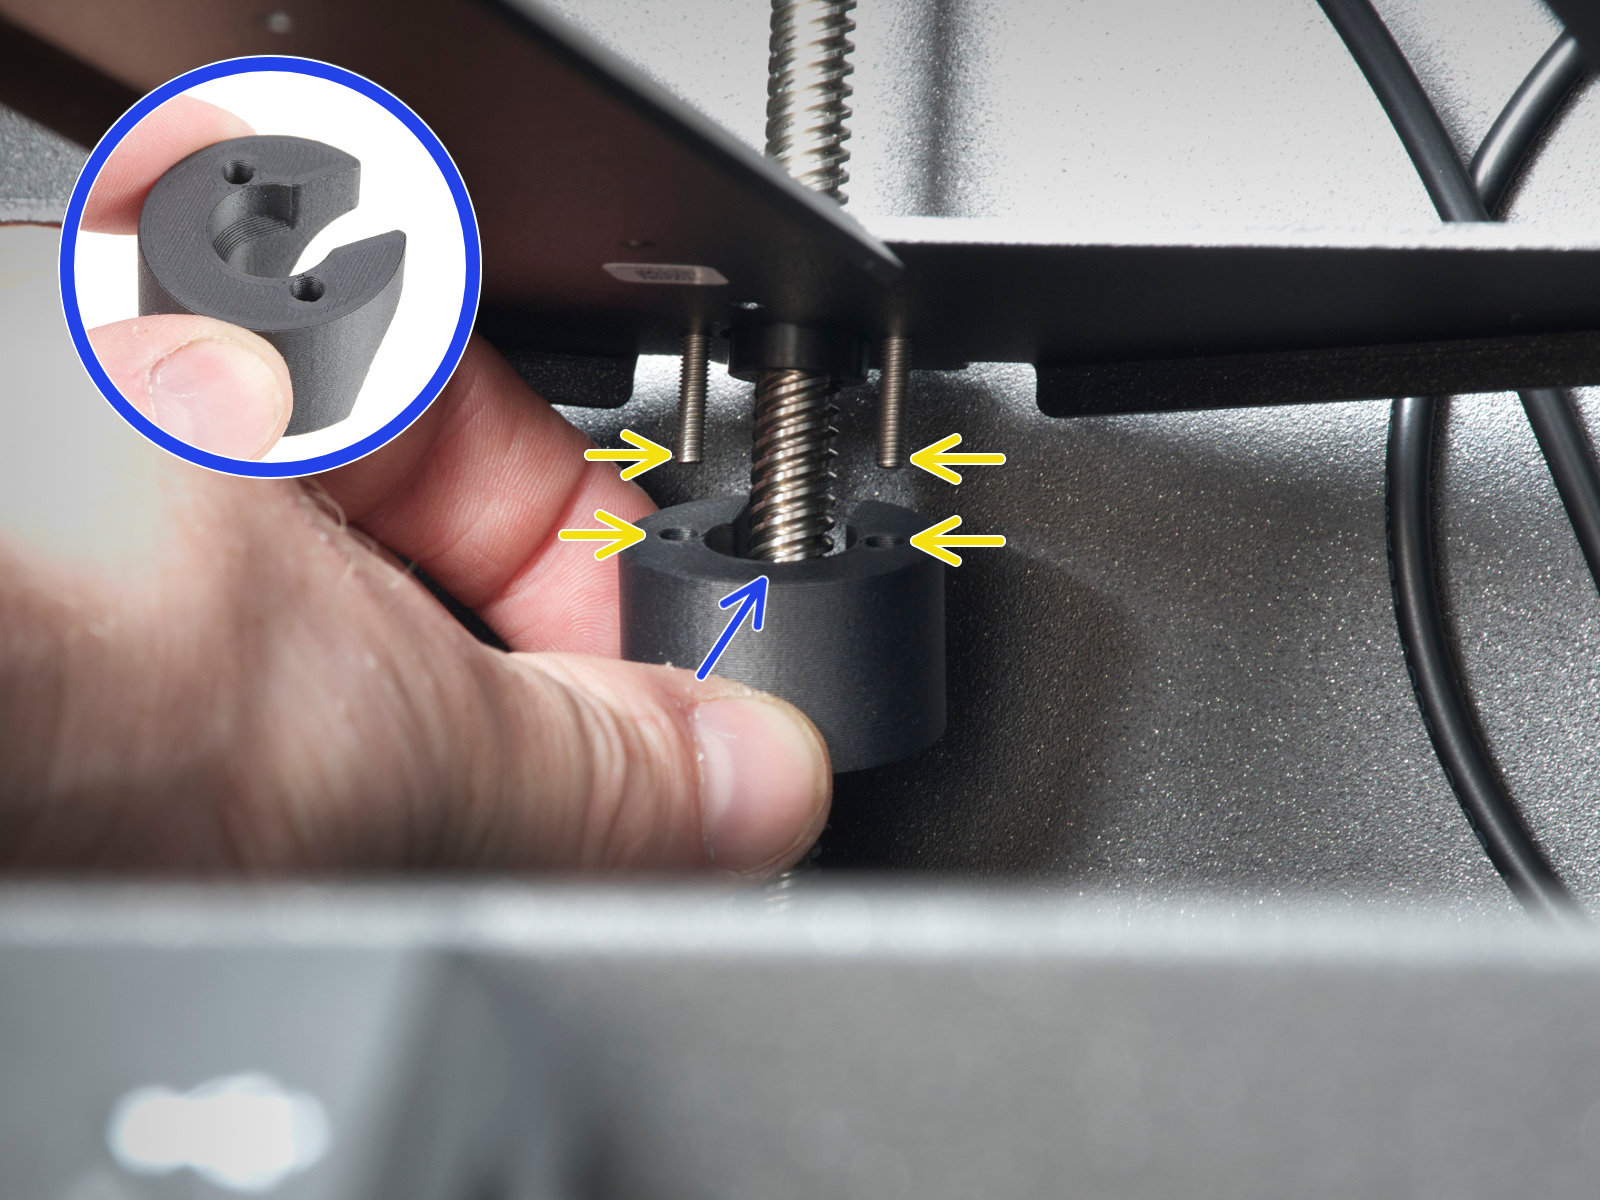
                  Check also that the spacers are correctly installed.
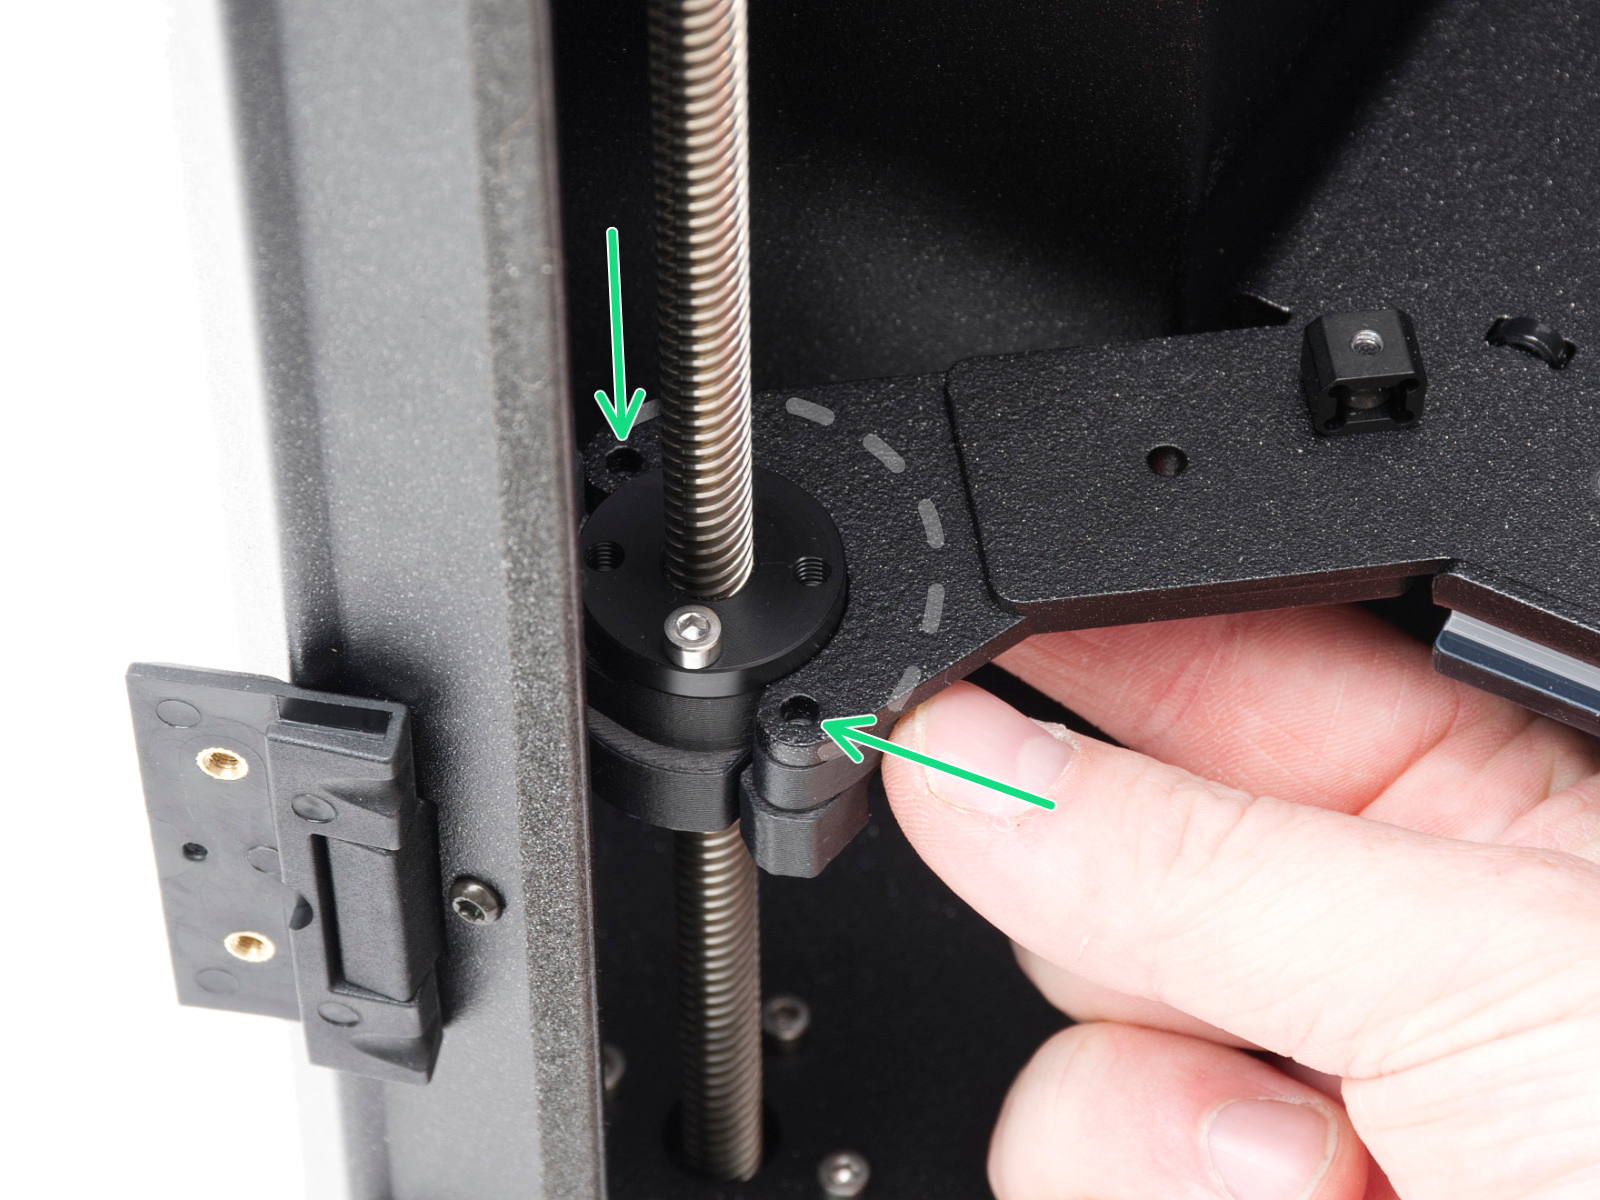
                  Left spacerRear spacerRight spacer

                  Belt tuning

                  The LCD menu will guide you through the belt wizard. If one of the sides shows a gap, do the following procedure:
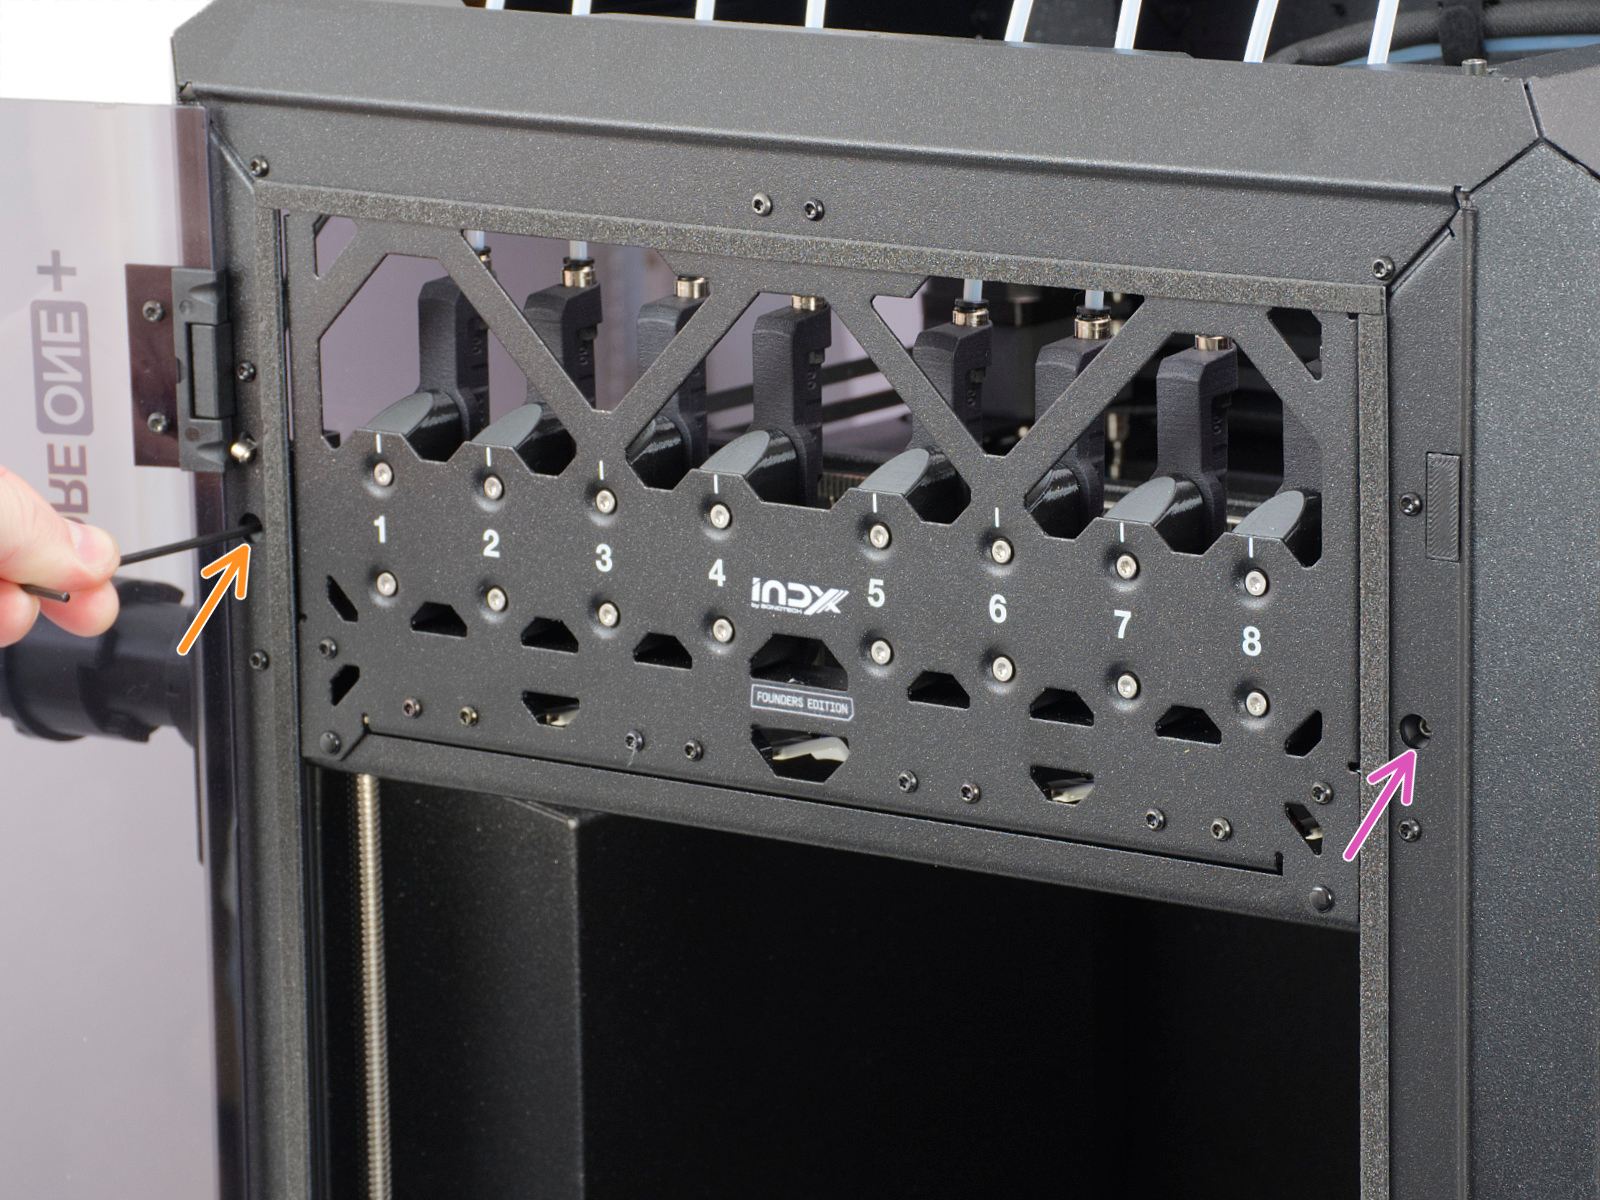
                  1. Loosen the belts completely. Be careful so that the square nuts do not fall off the plastic parts when removed.

                  1. Check which side sits against the back end (tight side) and which one has to be pushed towards it to touch it (loose side).
                  2. Put a universal wrench or anything with a similar thickness between the tight side and the back end. Slightly pull the loose side to correct the skew.
                  3. Check the alignment again and repeat if needed. In case the tight and loose sides switched, repeat the process from the other side, but apply a smaller amount of pressure.
                  4. Tighten the belts again.
                  5. Move the toolchanger around the Y and X axes by hand to even the belt tightness.

                  Homing calibration

                  If there are issues with the homing calibration, check the X and Y axes and the homing calibration again.

                  Dock calibration

                  This calibration will test each dock. If a specific dock fails, try:

                  • Tightening the dock screws further.
                  • Make sure that the toolchanger is fully pushed into the dock when requested.
                  • Redo the belt tuning and the homing calibration.

                  Loadcell test

                  A functioning loadcell is fundamental to detect that the nozzle is close enough to the steel sheet for printing, and to avoid damage that would be caused by the nozzle digging into the steel sheet.

                  Make sure that the surface the printer is on is as stable as possible: any form of vibration propagated to the surface under the printer, or a not fully stable surface under the printer, might cause a false reading on the loadcell, causing it to fail the selftest.

                  Check also if the main cable is properly connected to the toolchanger.

                  Z axis test

                  Check if there is anything blocking the path of the Z axis. It may be something stuck in the threaded rods or anything on the floor of the chamber.

                  Fan test

                  This part will test all fans in the printer. The RPM values for the fans need to be within these values for the test to pass:

                  • Print fan:  4800 - 6799 RPM
                  • Dock fan: 4800 - 6799 RPM
                  • Hotend fan: 12000 - 18000 RPM
                  • Chamber fan: 7225 - 9775 RPM
                  • Filtration fan: 2890 - 3910 RPM (for printers with the Advanced Filtration System)

                  If there is an error shown, first define which one of the fans has the issue.

                  Do not try to open the tool changer to access the hotend fan. You might damage the electronics inside.

                  The hotend fan is not accessible. To test it, go into the LCD menu to Control -> Temperature -> Nozzle, and set the nozzle to any temperature above 50 ºC. Check if you can hear the fan spinning. Then, go to the LCD menu in Info - Sensor Info - Fan Info, and check the hotend fan RPM.

                  If any of the other fans do not pass the test, check:

                  • Check for any obstruction that could prevent the fan from spinning. Particularly on the print fan, check if the cable is not going into the blades.
                  • Make sure that they are connected correctly to the electronics board.
                  • Go to the LCD menu in Control -> Temperature, and set the fan to be tested to 100%. See if the fan spins or if it shows any errors.

                  Heater test

                  The selftest can determine a fault during the heating of a component, and the affected component.

                  Heat the affected component under LCD Menu -> Control -> Temperature, heat up the part that failed the selftest, and see if any error appears. If it does, the error should have a QR code that redirects to the article that describes how to troubleshoot that particular error.

                  Tool offset calibration

                  If the tool offset calibration fails, check if all the nozzles are positioned correctly and the nozzle tips are clean.

                  Then, check the offset sensor for the following:

                  • The Prusa logo is facing up
                  • The cable is properly connected
                  • The board is secured

                  Also, try to redo the homing calibration.

                  Nozzle cleaner calibration

                  This calibration is a measurement and should not give any errors. In case the printer can't complete these tests, check the axes again.

                  Filament sensor calibration

                  The INDX has a side filament sensor. If the calibration fails, check the following:

                  • The 5x2 magnets are inserted and tightened
                  • The 7x8 magnets are in the correct orientation
                  • There is no filament debris in the filament sensor in the sensor case

                  Phase stepping calibration

                  For this test, make sure that you are not touching the printer and that no other printers are running on the same surface as the CORE One INDX. You can read more about it here: Phase Stepping (CORE One L, CORE One) [進行中の翻訳].

                  Input shaper calibration

                  After this calibration, the printer will show you the Input shaper frequency values. The lower limit is 35 Hz, and the upper limit is 70 Hz. If the value is too low or too high, check the belt tightness and the assembly.

                  この記事は役に立ちましたか?
                  この操作は登録ユーザーのみが利用できます。ログインしてください。
                  ログイン してコメントを投稿する
                  コメントなし

                  トピックス

                  • トラブルシューティング
                    • プリンタートラブルシューティング
                      • ヒートベッドポートの過電流 #26309 (MK4S) #13309 (MK4) #27309 (MK3.9S) #21309 (MK3.9) #28309 (MK3.5S) #23309 (MK3.5) #31309 (CORE One)
                      • ロードセル測定の失敗 #31526 (CORE One) #26526 (MK4S) #13526 (MK4) #27526 (MK3.9S) #21526 (MK3.9)
                      • Nozzle Timeout #31819 (CORE One) #35819 (CORE One L) #36819 (CORE One INDX) #26819 (MK4S) #13819 (MK4) #27819 (MK3.9S) #21819 (MK3.9) #28819 (MK3.5S) #23819 (MK3.5) #17819 (XL) #12819 (MINI)
                      • Chamber overheating #36260 (INDX) #31260 (CORE One) #35260 (CORE One L) #17260 (XL)
                      • Chamber temperature is critical #36261 (INDX) #31261 (CORE One L) #35261 (CORE One) #17261 (XL)
                      • Selftest failed (CORE One INDX)
                    • Diagnostics [進行中の翻訳]
                    • プリント品質のトラブルシューティング
                    • QR Error codes [進行中の翻訳]
                    • プリントエラーメッセージ