Prusa
  • SHOP
    • Latest products
    BY CATEGORY
    • 3D printersnew
    • 3D printer upgradesnew
    • Materials
    • Accessories
    • Spare parts
    • Courses
    • Merch
    • Get a price quote
    QUICK LINKS
    • Shipping & delivery
    • Returns & refunds
    • Payment & financing
    • Warranty
    • VAT & Customs fees
    • FAQ

    0 item in your cartitems in your cart

    Your cart is empty

    Go to cartShop 3D printers

    My profile

    Log in to see orders, saved items

    My profile

    Signed in as

    • Orders
    • Logout
  • 3D PRINTING
    • Explore 3D printing
    FOR BEGINNERS
    • 3D printing 101
    • How FDM printing works
    • Buying your first printer
    • 3D model catalog
    BY APPLICATION
    • Rapid prototyping
    • Manufacturing
    • Engineering
    • Research
    • Arts & design
    GO DEEPER
    • Materials guide
    • Courses
    • Webinars
    • Case studies
    • Custom 3D printing
  • 3D PRINTERS
    • All 3D printers
    FOR
    • Home or garageHobbyists, tinkerers and home printing
    • BusinessIn-house production for small teams
    • EnterpriseFleets, security and scale
    • Which Prusa is right for me
    SHOP & BROWSE
    • CORE One+new
    • CORE One+ INDXnew
    • CORE One L+new
    • CORE One L+ INDXnew
    • XL+new
    • MK4S
    • Prusa Pro HT90
    • Prusa Pro AFS
    • Prusa Pro SLX
    MORE FROM PRINTERS
    • Parts & upgradesnew
    • Spare parts
    • Critical infrastructure
    • Case studies
    • Signature Oak
    • Kits
  • MATERIALS
    • All materials
    BY USE
    • Every-day & design
    • Functional engineering
    • Composites
    • Pro speciality
    • SLA resins
    PRUSAMENT
    • PLA
    • PETG
    • ASA
    • PC
    • PA11
    • Flex
    • TPU
    MORE FROM MATERIALS
    • Materials guide
    • We make material in house
    • Sustainability
    • Order on the store
  • SOFTWARE
    • All software
    PREPARE THE PRINT
    • PrusaSlicer 3.0New
    PRINT & MONITOR
    • Prusa Connect
    • EasyPrint
    • iOS & Android app
    • Prusa Farm
    GET STARTED
    • Download & install
    • Knowledge base
    MORE FROM SOFTWARE
    • 3D model catalog
  • SUPPORT
    • Explore support
    FIND ANSWERS
    • Knowledge base
    • Troubleshooting
    • Courses
    • Webinars
    GET HELP
    • Contact us
    • Livechat
    • Shipping & delivery
    • Warranty
    • Returns & refunds
    • Service & spare parts
    • Service & Repair
    COMMUNITY
    • Forum
    • Reddit
    • Printables
  • TRUST CENTER
    • Trust Center overview
    BY TOPIC
    • GDPR
    • Certificates
    • Security
    • Compliance
    COMMITMENTS
    • Sustainability report
    TALK TO US
    • Contact the security team
  • COMPANY
    • About Prusa
    GET TO KNOW US
    • Our story
    • How we make printers
    • Open source
    • Brand & media kit
    NEWS
    • Blog
    • Newsroom
    • Events
    TRUST & PARTNERS
    • Sustainability
    • Resellers & distributors
    • Affiliate program
    • Contact
    • English
    • Čeština
    • Deutsch
    • Español
    • Français
    • Italiano
    • Polski
    • 日本語
  • Signed in as

    • Orders
    • Address
    • In-stock Alerts
    • My Courses
    • Subscription
    • Edit Account
    • Logout

Log in to see orders, saved items

Signed in as
  • Orders
  • Address
  • In-stock Alerts
  • My Courses
  • Subscription
  • Edit Account
  • English
  • Čeština
  • Deutsch
  • Español
  • Français
  • Italiano
  • Polski
  • 日本語
Shop

0 item in your cartitems in your cart

Your cart is empty

Go to cartShop 3D printers

My profile

Log in to see orders, saved items

My profile

Signed in as

  • Orders
  • Logout
SHOP
  • Latest products
BY CATEGORY
  • 3D printersnew
  • 3D printer upgradesnew
  • Materials
  • Accessories
  • Spare parts
  • Courses
  • Merch
  • Get a price quote
QUICK LINKS
  • Shipping & delivery
  • Returns & refunds
  • Payment & financing
  • Warranty
  • VAT & Customs fees
  • FAQ

Featured products

    Popular categories

      Trending searches

        Articles

          Blog

            Products

              Categories

                Suggested searches

                  Searching…
                  No results
                  Something went wrong.
                  ↑↓ Select↵ OpenEsc Close search
                  1. Support
                  2. Print settings
                  3. Max volumetric speed
                   

                  Contents

                  • What determines the final print speed?
                  • Print MVS vs Filament MVS
                  • Autospeed
                  • Choosing MVS
                  • Preview MVS

                  Blog

                  • Prusament Pellets: Raw material batches for large-format 3D printing or small-scale polymer research & development
                  • Print colorful and glowing Halloween decorations with our spooky offer
                  • Factorio Has Arrived on Printables

                  Newsletter

                  Signup and get our monthly squeeze on updates, blog, printables and much more.

                  By clicking, you agree to receive our newsletter.

                  This site is protected by reCAPTCHA Enterprise and the Google Privacy Policy and Terms of Service apply.

                  Heavy Duty Keyboard Holder (No Supports)
                  E-shop
                  • 3D Printers
                  • Printer Upgrades
                  • Filaments
                  • Accessories
                  • Prusa Merchandise
                  Prusa

                  © Prusa Research a.s.

                  Printables
                  • 3D Models
                  • Store
                  • Clubs
                  • 3D Design Contests
                  • Brands
                  Community
                  • World Map
                  • Forum
                  • User Groups
                  • Events
                  Help
                  • Prusa Help
                  • Prusa Academy
                  • 3D Printing Calculators
                  Software
                  • PrusaSlicer
                  • Prusa.app
                  • Prusa Connect
                  • Drivers and Software
                  Company
                  • About Us
                  • Blog
                  • Official Prusa Resellers
                  • Contact Us
                  • Certified for ISO 9001, ISO 14001, ISO 45001
                  • General Terms and Conditions
                  • General Terms and Conditions of Use of the PRUSA Websites
                  • Privacy Policy
                  • Information about cookies
                  • Customer Complaints Policy
                  • Status Page
                  • Do Not Sell or Share My Personal Information
                  • Supplemental Statements
                  Prusa
                  • General Terms and Conditions
                  • General Terms and Conditions of Use of the PRUSA Websites
                  • Privacy Policy
                  • Information about cookies
                  • Customer Complaints Policy
                  • Status Page
                  • Do Not Sell or Share My Personal Information
                  • Supplemental Statements

                  © Prusa Research a.s.

                  JOSEF PRUSA®, PRUSA RESEARCH®, PRUSA POLYMERS®, PRUSA ORANGE®, PRUSA 3D ® AND PRUSAMENT® are registered trademarks of Prusa Development a.s. used by Prusa Research a.s. under licence from Prusa Development a.s.

                  Max volumetric speed

                  Relevant for

                  MMU family
                  MK3 family
                  OLD PRODUCTS
                  SOFTWARE
                  19 comments
                  Article is also available in following languages
                  English
                  Čeština
                  Polski
                  Deutsch
                  Français
                  Español
                  Italiano
                  日本語

                  The Maximum volumetric speed setting (MVS), sometimes referred to as AutoSpeed, is one of the most powerful features in PrusaSlicer. MVS is the maximum amount of plastic (mm³/s) your hotend can reliably melt. Think of it as a speed limiter: PrusaSlicer lets your requested speeds through when safe, and only reduces them when the hotend would be asked to melt more than it can handle.

                  With MVS set correctly, you don't need to manually calculate safe speeds for every nozzle/layer height combination. MVS never increases your speed, it can only reduce it.

                  This gives PrusaSlicer users a significant advantage. Instead of trying to calculate ranges of speeds for combinations of nozzle sizes, layer heights, or extrusion widths, you can specify the speeds and settings you desire, then let MVS regulate speeds at slice time when necessary.

                  What determines the final print speed?

                  During printing, each extrusion move checks multiple limits. The most restrictive one among those will be used:

                  • Per-Feature Speed: your configured speed for each extrusion type in Print Settings - Speed (e.g., Perimeter speed, Infill speed, Bridge speed). Setting any of these to 0 mm/s activates automatic speed calculation for that type (see Autospeed).
                  • Max Volumetric Speed: if the requested speed exceeds the MVS, it is reduced. Wider/taller extrusions get slowed down more. The calculation used for the max speed is Max speed = MVS / cross-section area. PrusaSlicer uses a stadium-shaped cross-section model for accurate volume calculation.
                  • Overhang & Cooling: overhanging perimeters are slowed down based on how unsupported they are.
                  • Layer Time Cooldown: if the total layer time is too short, all speeds are reduced proportionally. The lowest speed possible is the one from Min Print Speed.
                    Set MVS to zero (0) for no limit.

                  Print MVS vs Filament MVS

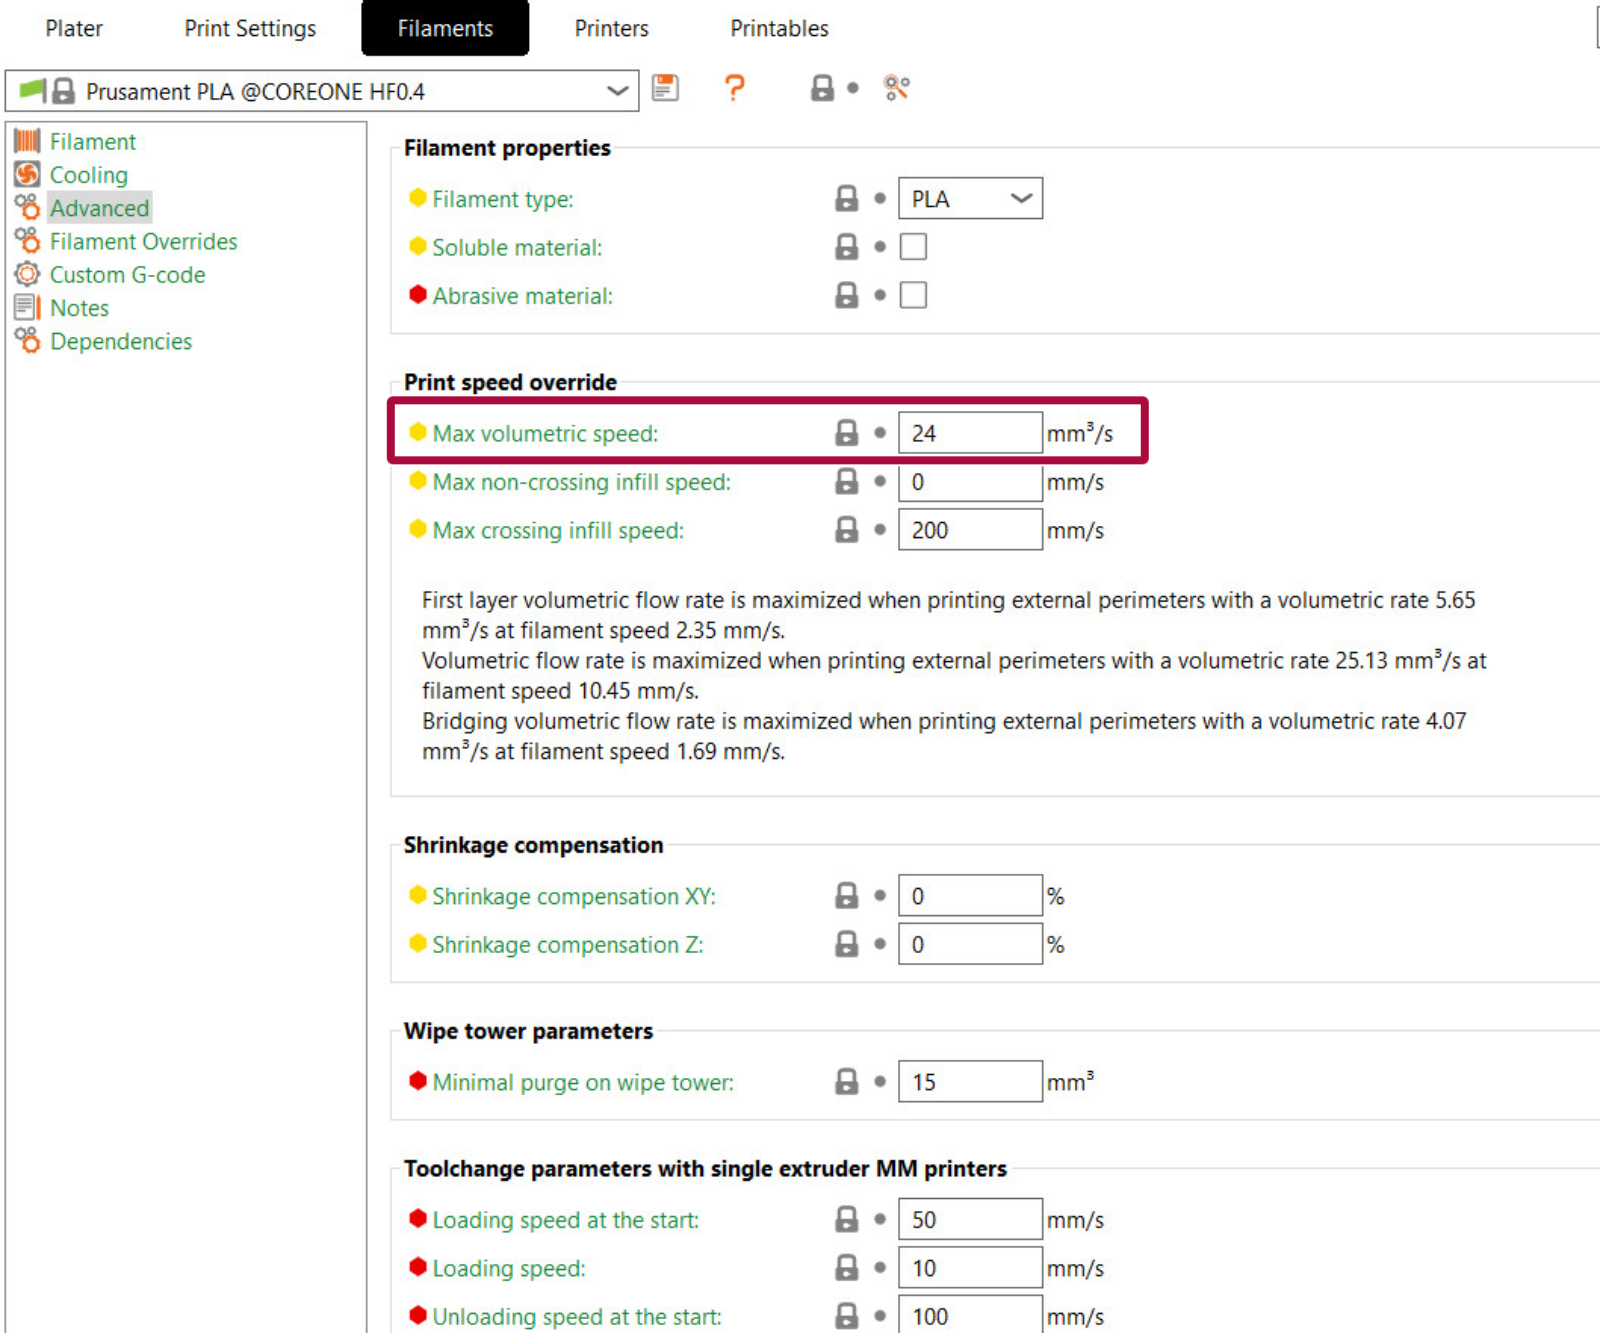
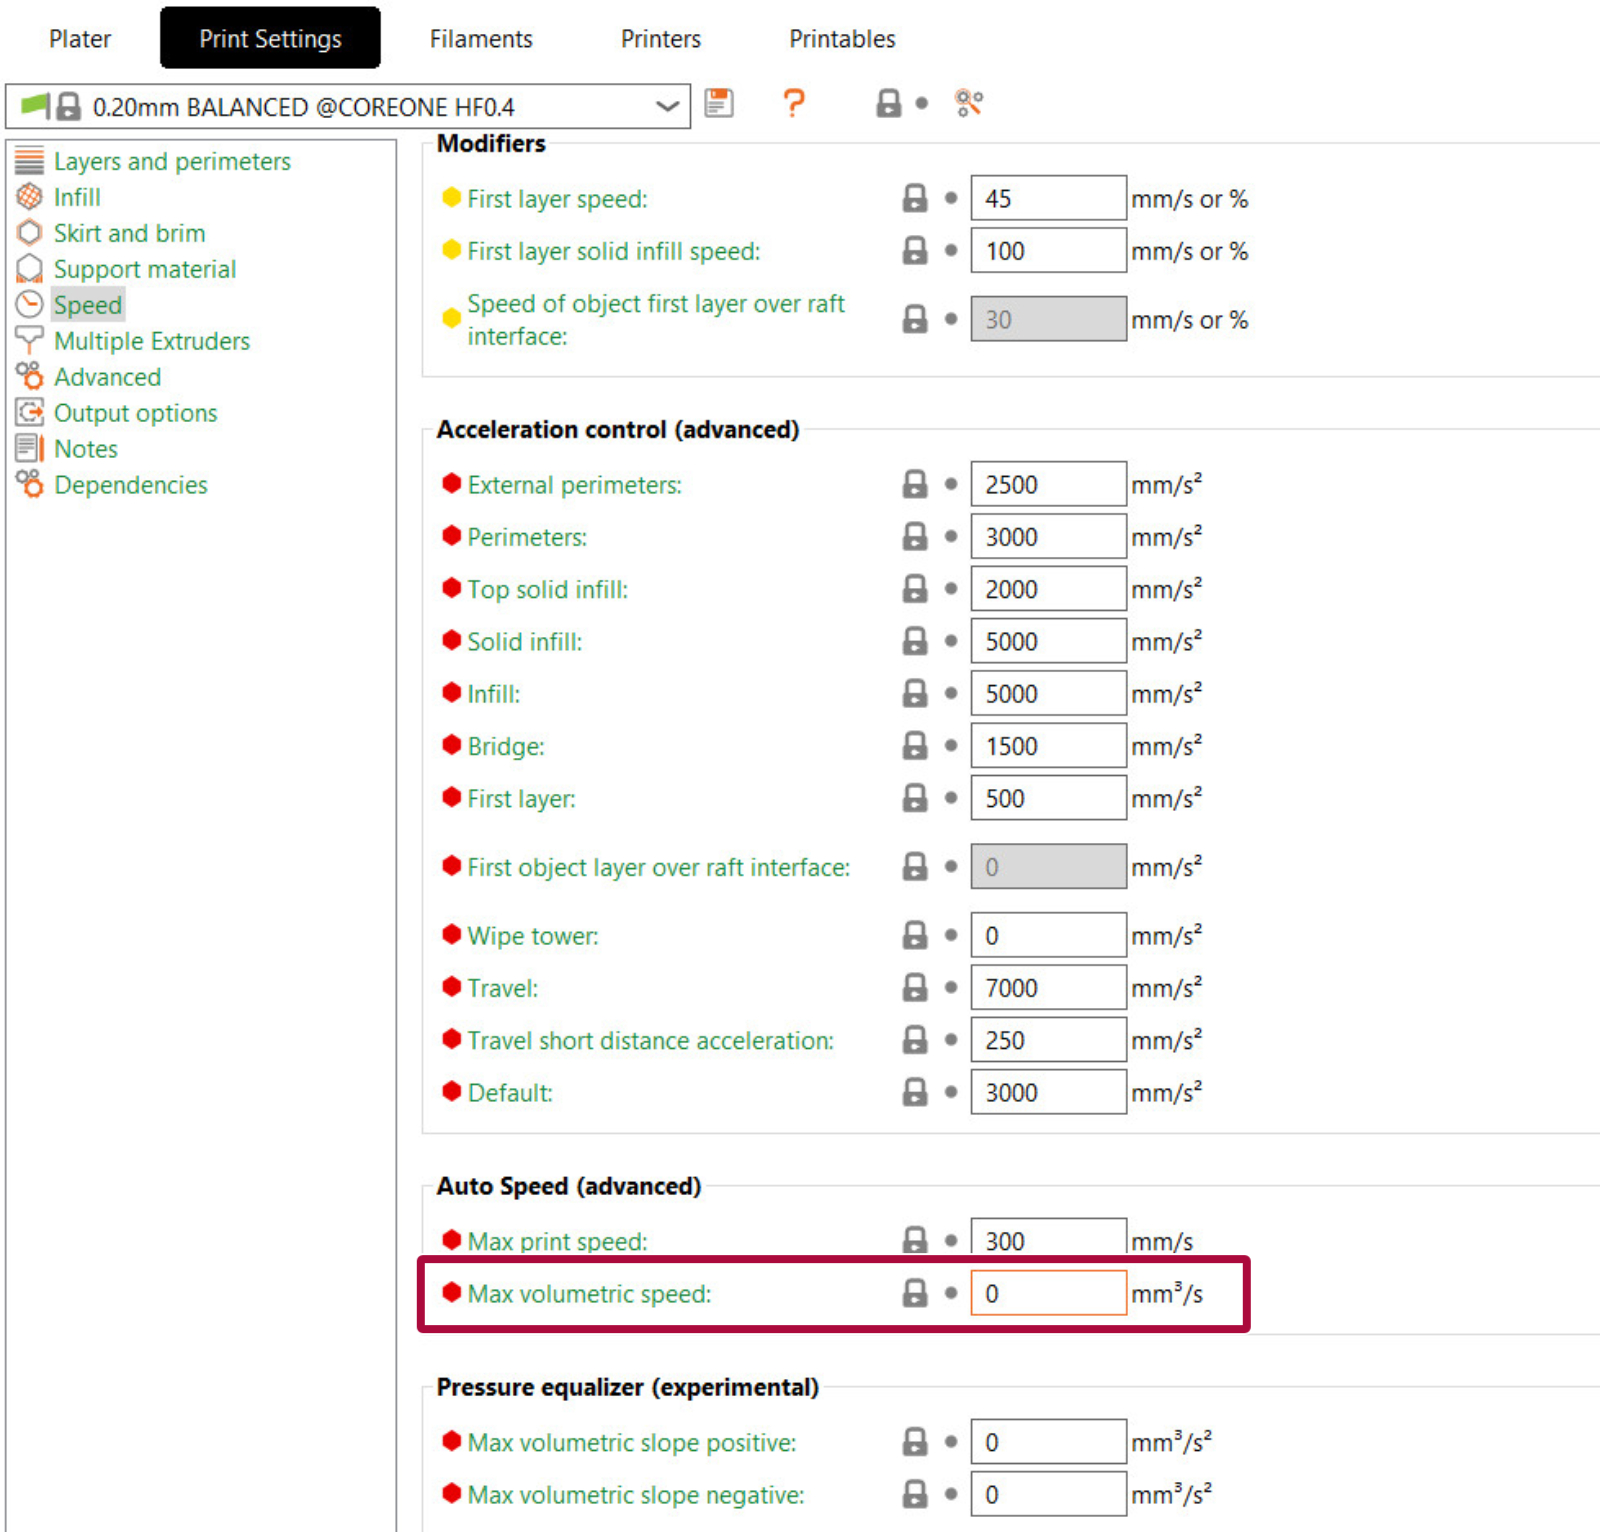
                  It is possible to set the MVS in two places in PrusaSlicer: Print settings -> Speed -> Max volumetric speed and Filament settings -> Advanced -> Max volumetric speed. The value chosen will always be the lowest between the two. Setting either to 0 disables that limit and uses the other one.
                  Autospeed

                  Setting any print speed setting (e.g., Perimeter speed, Infill speed) to 0 mm/s activates AutoSpeed for that extrusion type. MVS stops being just a brake and becomes the basis for calculating speed.

                  PrusaSlicer finds the smallest extrusion cross-section among all extrusion types with speed set to 0, multiplies it by Max Print Speed (found in Print Settings -> Speed -> Max print speed), and caps the result with MVS. Each extrusion then gets: "target volumetric speed / its cross-section". Thinner extrusions print faster, thicker ones slower. Note that Max Print Speed is used only in AutoSpeed mode, and it has no effect when speeds are non-zero.

                  AutoSpeed activates per extrusion type. For example, setting the Infill speed to 0 auto-calculates only infill, while perimeters still use their configured value.

                  Note that ironing extrusions are excluded from the calculation.

                  Choosing MVS

                  The correct MVS value depends on your hotend and the material you are printing with. Start conservative and increase gradually. Signs of MVS being too high: extruder clicking, under-extrusion at high speeds, poor layer adhesion.

                  The effective MVS is limited by the weaker link, either the hotend or the material. Set each in its respective profile, and PrusaSlicer will use the lowest value.

                  The effective MVS is limited by the weaker link, either the hotend or the material. Set each in its respective profile, and PrusaSlicer will use the lower value.

                  Filaments

                  Different filament materials have different characteristics. Viscosity, stiffness, and other factors may greatly reduce effective throughput.

                  FilamentTypical MVS RangeNotes
                  PLA12–20 mm³/sEasy to melt, higher flow possible
                  PETG8–15 mm³/sSlightly more viscous than PLA
                  ABS/ASA10–16 mm³/sSimilar to PETG
                  TPU2–5 mm³/sFlexible filaments require very
                  low flow
                  PC6–10 mm³/sHigh viscosity, slow melting
                  PA (Nylon)8–12 mm³/sVaries widely by blend

                  Hotend

                  HotendTypical MVS Range
                  Standard all-metal (e.g., E3D V6, Prusa MK3 stock)8–12 mm³/s
                  Prusa Nextruder (MK4/XL)15–20 mm³/s
                  High-flow nozzles (CHT, Bondtech CHT)20–35 mm³/s
                  High-flow hotends (Revo High Flow, Rapido HF)25–40 mm³/s

                  Nozzle diameter

                  Intuitively, it may seem that the nozzle diameter shouldn't affect the maximum amount of plastic that the hotend can heat in a given amount of time. However, with bigger nozzles, you can slightly increase MVS due to lower mechanical resistance - basically, it's a bit easier for the filament to get pushed through the nozzle.

                  And vice versa, with smaller nozzles, you'll have to decrease MVS a bit.

                  With larger nozzles, consider increasing the nozzle temperature to allow for even bigger MVS. E.g., you can print PLA 10-20 °C hotter than our standard profile when using a 0.6 mm nozzle.
                  Does printing with a large diameter nozzle and tall layer height actually save print time?

                  This is an often-overlooked consequence of MVS. When you use a large diameter nozzle and a very tall layer height, e.g., a 0.8 mm nozzle and a 0.5 mm layer height, your print speed is indeed going to be capped by MVS. That is, unless you install a more powerful hotend on your printer. If you notice in the preview that your speed is limited by MVS, you can try increasing the nozzle temperature and raising MVS a bit. However, it may be time to simply lower the layer height. You'll get more detail without increasing the print time because the printer will be able to print faster.

                  Preview MVS

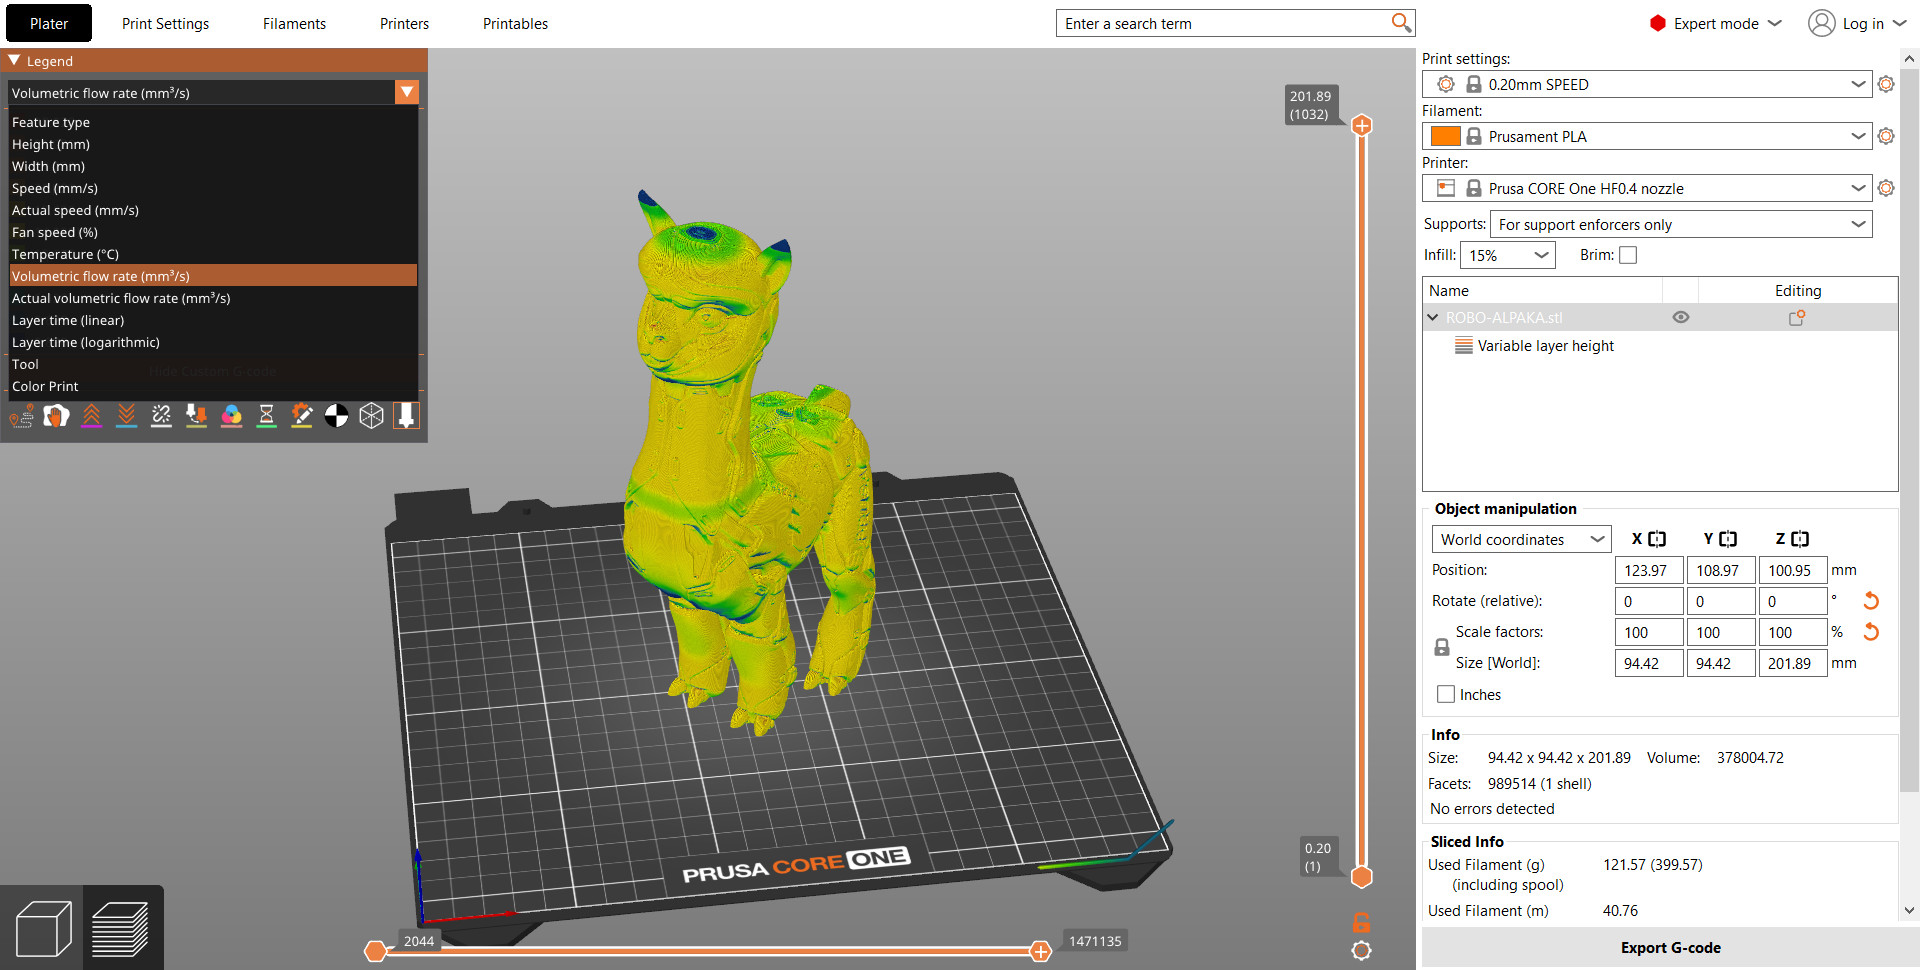
                  Once you slice your model, you can switch the preview mode to Volumetric flow rate using the select box on the top left corner.

                  On smaller models, you'll notice you're not being capped by MVS at all. Likewise, if you're printing with a small layer height, you're most likely not going to be capped by MVS. 

                  On the other hand, when printing bigger models with tall layer heights, you may notice the speed being limited by MVS, especially when printing infill. If the majority of your model is being printed more slowly due to the MVS limit, consider lowering the layer height. You'll get more details "for free".
                  Big thanks to Bob George for his help on this article

                  Was this article helpful?
                  This action is available only to registered users. Please log-in.

                  Topics

                  • PrusaSlicer 2.9 (Legacy)
                    • Print settings
                      • Infill
                      • Support material
                      • Layers and perimeters
                      • Elephant foot compensation
                      • Sequential printing
                      • Max volumetric speed
                      • Skirt and Brim
                      • Ironing
                      • Fuzzy skin
                      • Slicing mode / 3DLabPrint airplanes
                      • Pressure equalizer
                      • Arachne perimeter generator
                      • Organic Supports
                      • Speed settings
                      • Infill patterns
                      • Seam position
                    • About PrusaSlicer
                    • Configuration and profiles
                    • User interface
                    • Input/output
                    • Left toolbar
                    • Top toolbar
                    • Filament settings
                    • Printer settings
                    • Advanced features
                    • Multi-material slicing
                    • SLA slicing
                    • Other (PrusaSlicer)

                  14 comments

                  Log in  to post a comment
                  raporter1992
                  •
                  spoke with prusa technical support about this. I inquired about two specific printers. The MK4s and the Core One+. As of the writing of this comment:

                  max speed - 300
                  flow rate - 24mm3/s on HF nozzles, and 15mm3/s on the regular (non-HF) nozzles --calculated for PLA example (so set these numbers as your max depending on if you use a high flow nozzle or regular nozzle and then use filaments settings to use a smaller number based on the filament type)
                  Reply
                  Harris
                  •
                  Yep this badly needs an update, also with figures for (eg) Nylon & Polypropylene.
                  Reply
                  George
                  •
                  We need updated numbers now with core xy printers and high flow nozzles...
                  Reply
                  jimwsmith
                  •
                  On blurb when MK4S was released this was siad:
                  a Bondtech CHT nozzle that increases Volumetric Flow. The new nozzle pushes ordinary Prusament PLA out with a volumetric flow of 24mm³, which is a 50% increase from the MK4 standard of 16mm³
                  Reply
                  bryn51
                  •
                  This article is useful, but it needs to be updated to include information about the newer model printers : Mk4, Mk4S, CoreOne and XP, plus impact of CHT Nozzles.
                  It would also be useful to know how Prusa Slicer arbitrates between Print Profile Autospeed settings (Max volumetric speed) and Filament Profile MVS.
                  Reply
                  Otmar
                  •
                  100% agree
                  Reply